Welding Positioner in Chennai
Cyclotron Manufactures the Best Welding Positioner in Chennai, Tamil Nadu. We serve the region and have customers from Ambattur, Oragadam, Sriperumbudur, Irungattukottai, Gummidipoondi, Manali, and Thiruvallur region
We are manufacturers, not resellers. That means you can speak directly with the team that builds your machine, understand its capabilities and see it working before you make a purchase.
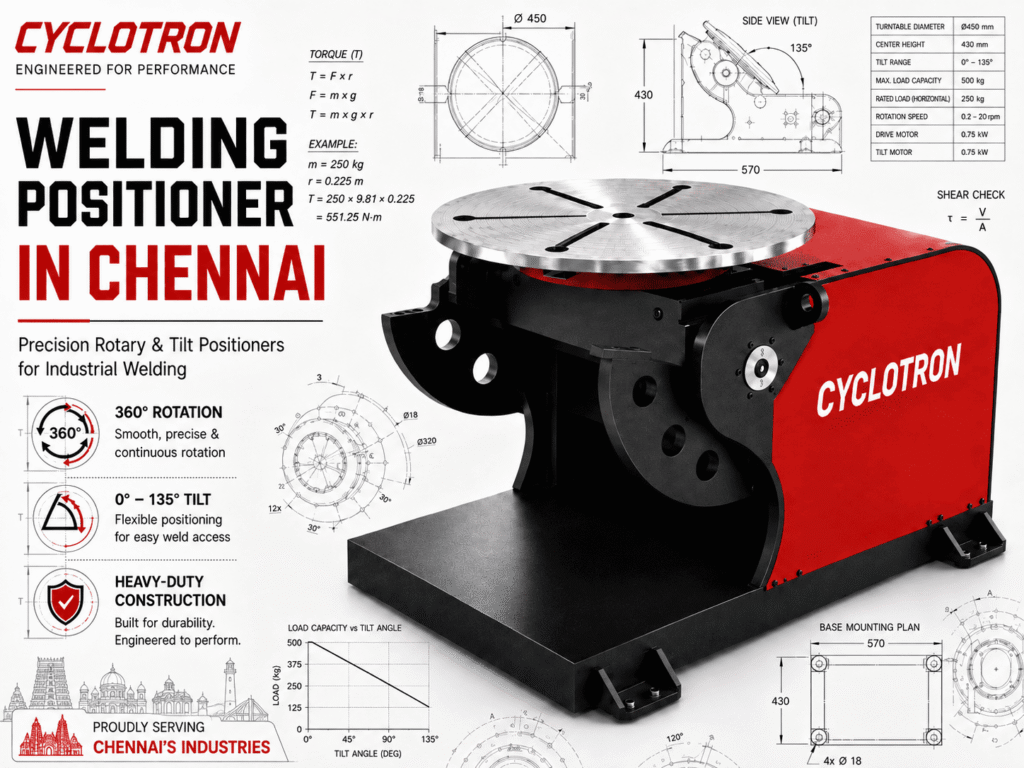
Welding positioner manufacturer in Chennai
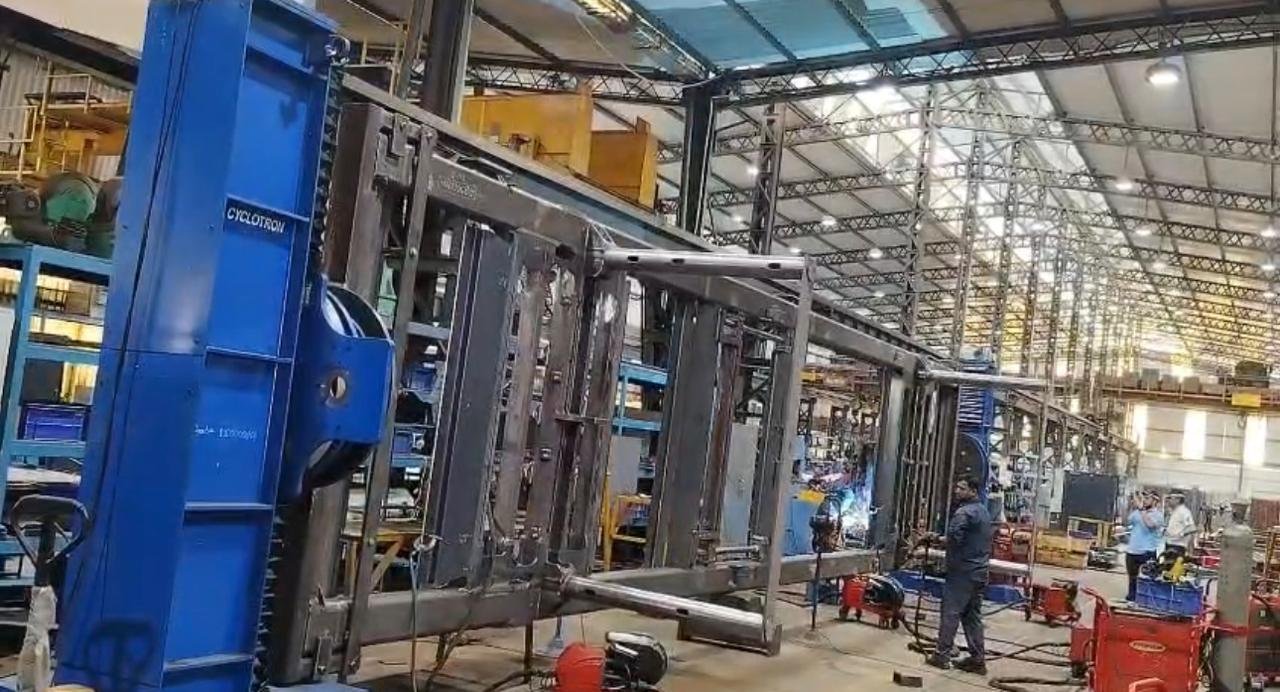
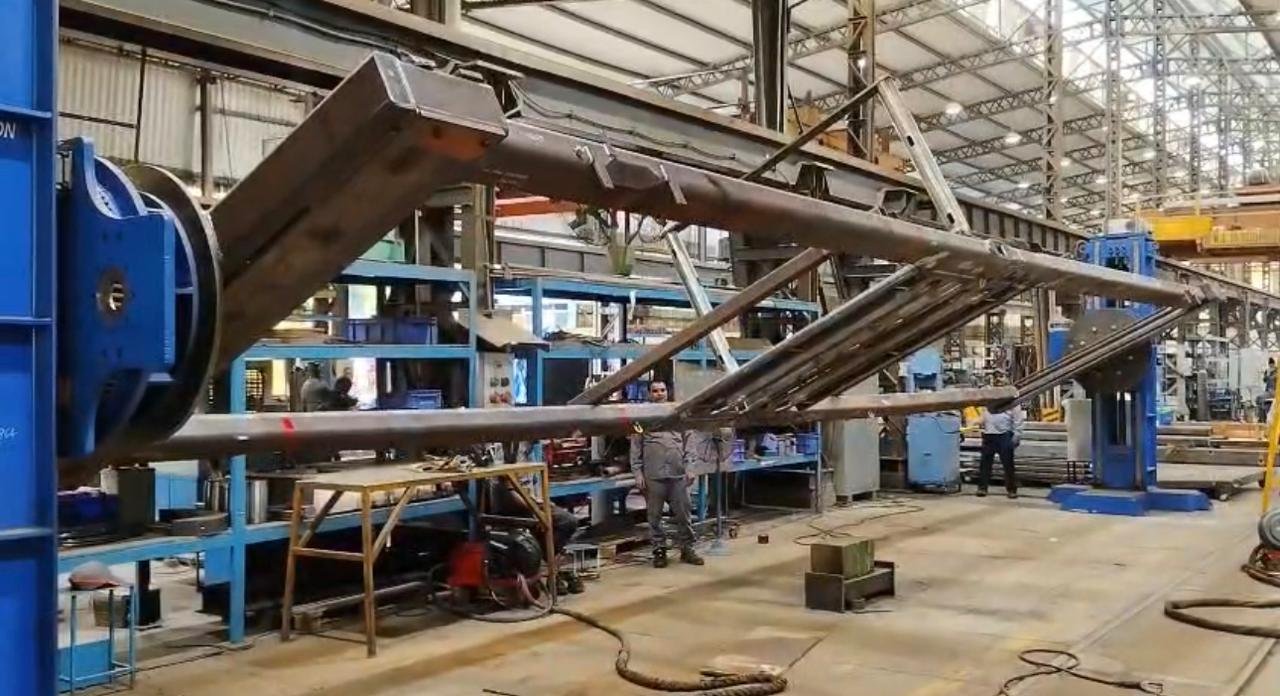
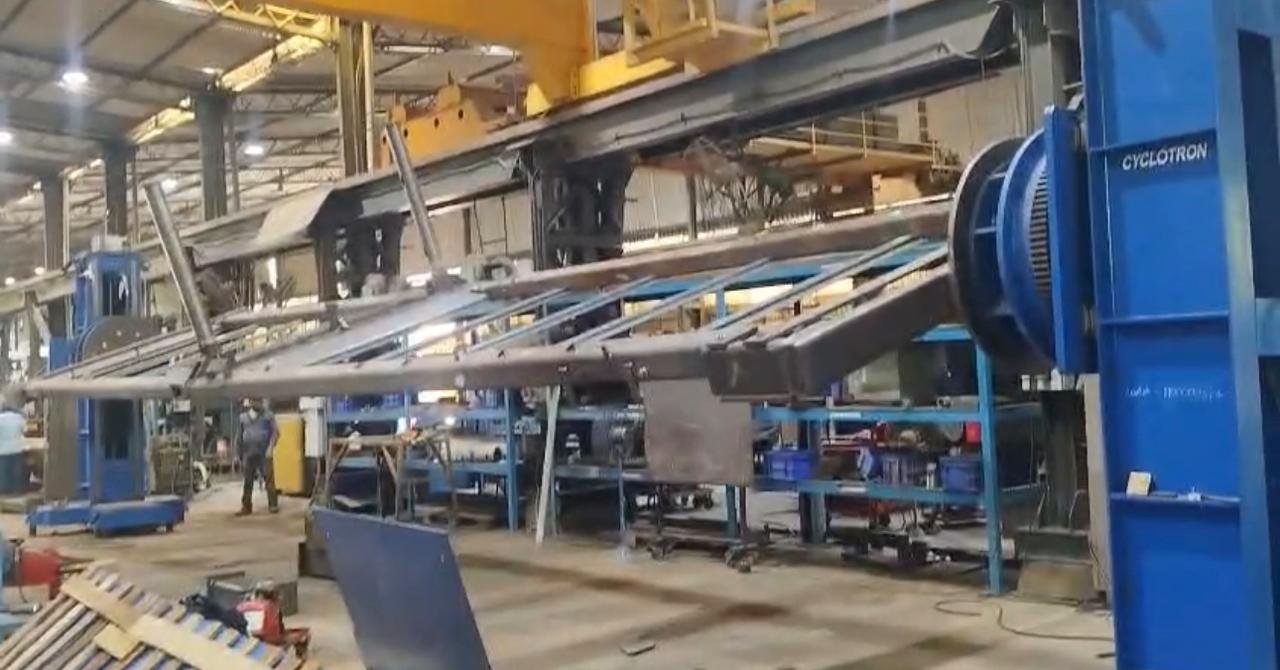
Cyclotron manufactures industrial welding positioners from 100 kg to 100 Tons capacity, designed for robotic/manual welding, heavy fabrication, and high-production welding environments.
500+
Successfully Project Finished.
7+
Years of experience with proud
100+
Companies worldwide
50+
Colleagues & counting more daily
Welding positioner manufacturer in Chennai
When you are producing hundreds of welded components, a few minutes saved on every part can become hours saved every shift. That is why Chennai buyers look at a welding positioner differently. The question is not simply whether it can rotate the component but how much handling time can it remove from every cycle?
We supply welding positioners for high-volume fabrication across Ambattur, Oragadam, Sriperumbudur, Irungattukottai, Gummidipoondi, Manali, and Thiruvallur. From automotive and railway fabrication to heavy engineering, our focus is on helping production teams improve cycle time, operator utilisation, and throughput.
Trusted By Industry Leaders from Bangalore
Rotary welding positioner in Chennai
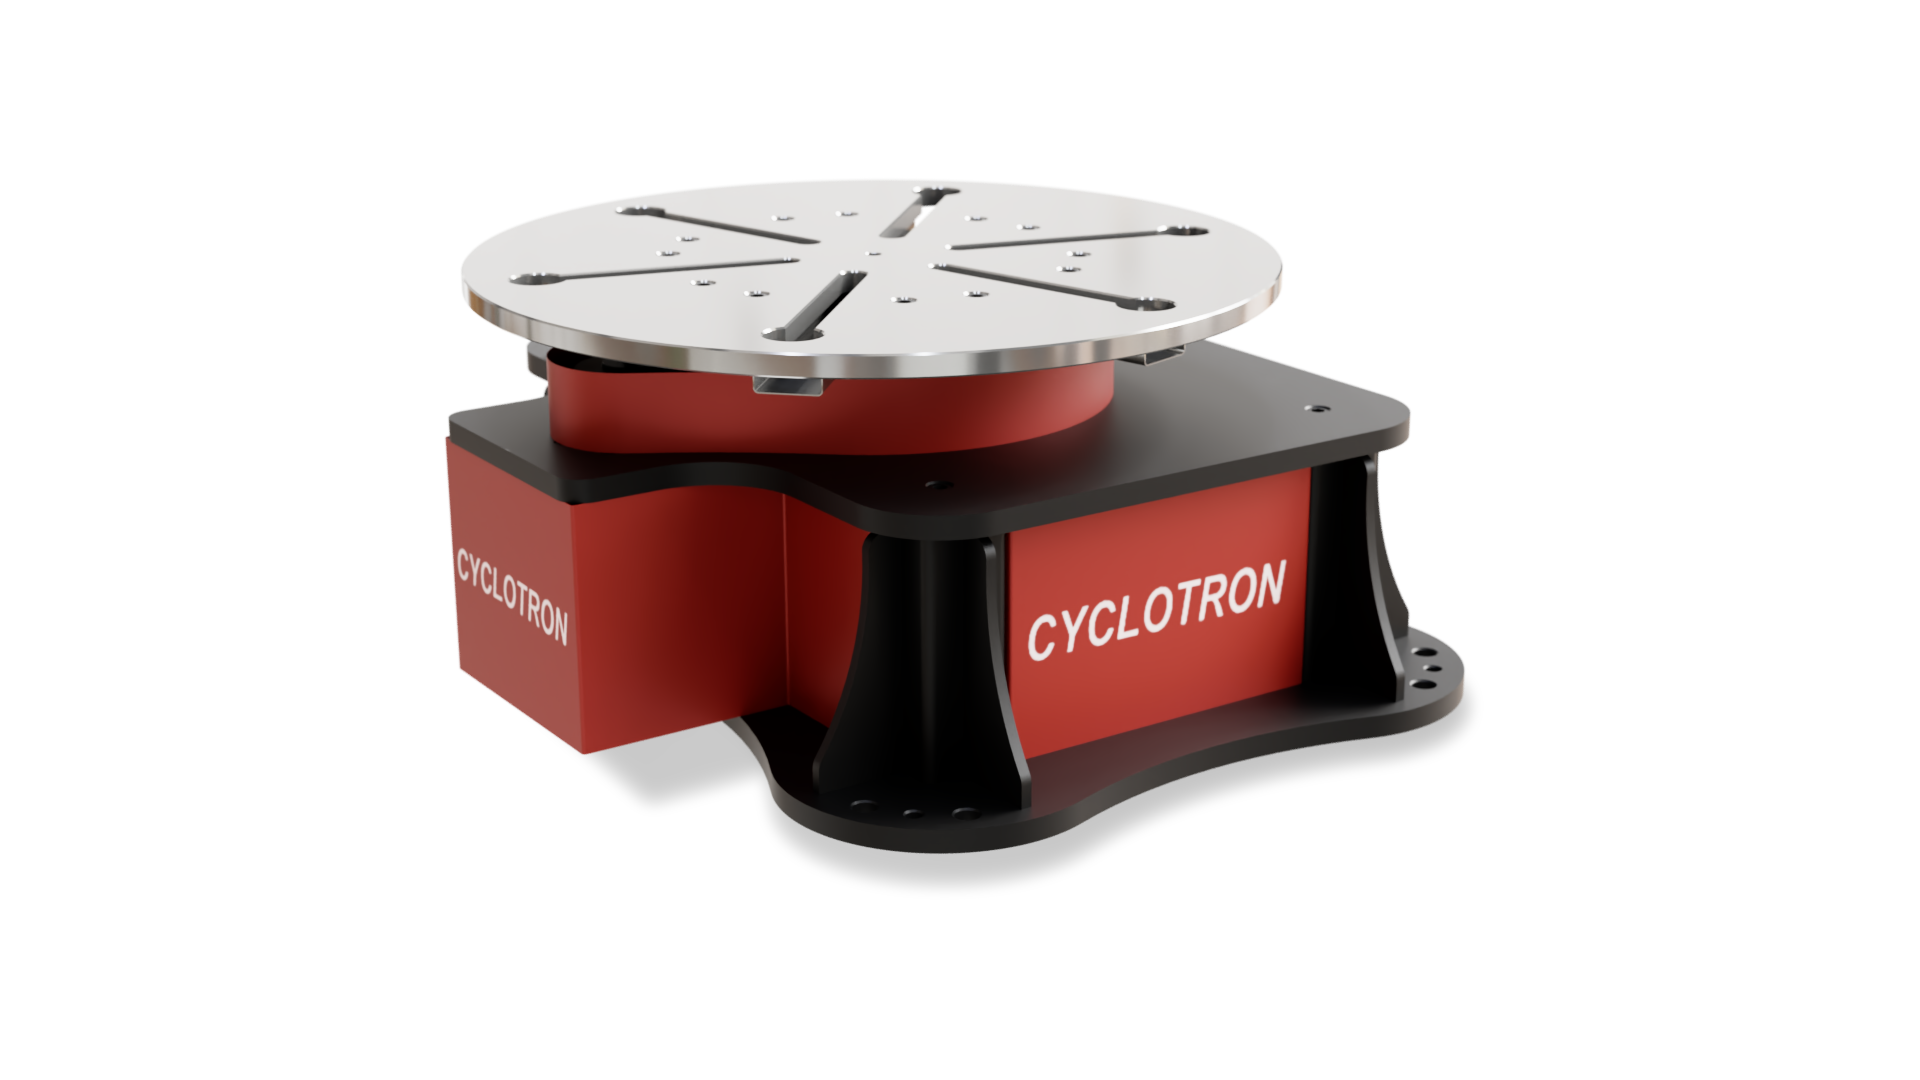
Welding turntable
SKU: CTT-1AX
1st Axis: Face plate Rotation (0-360°)
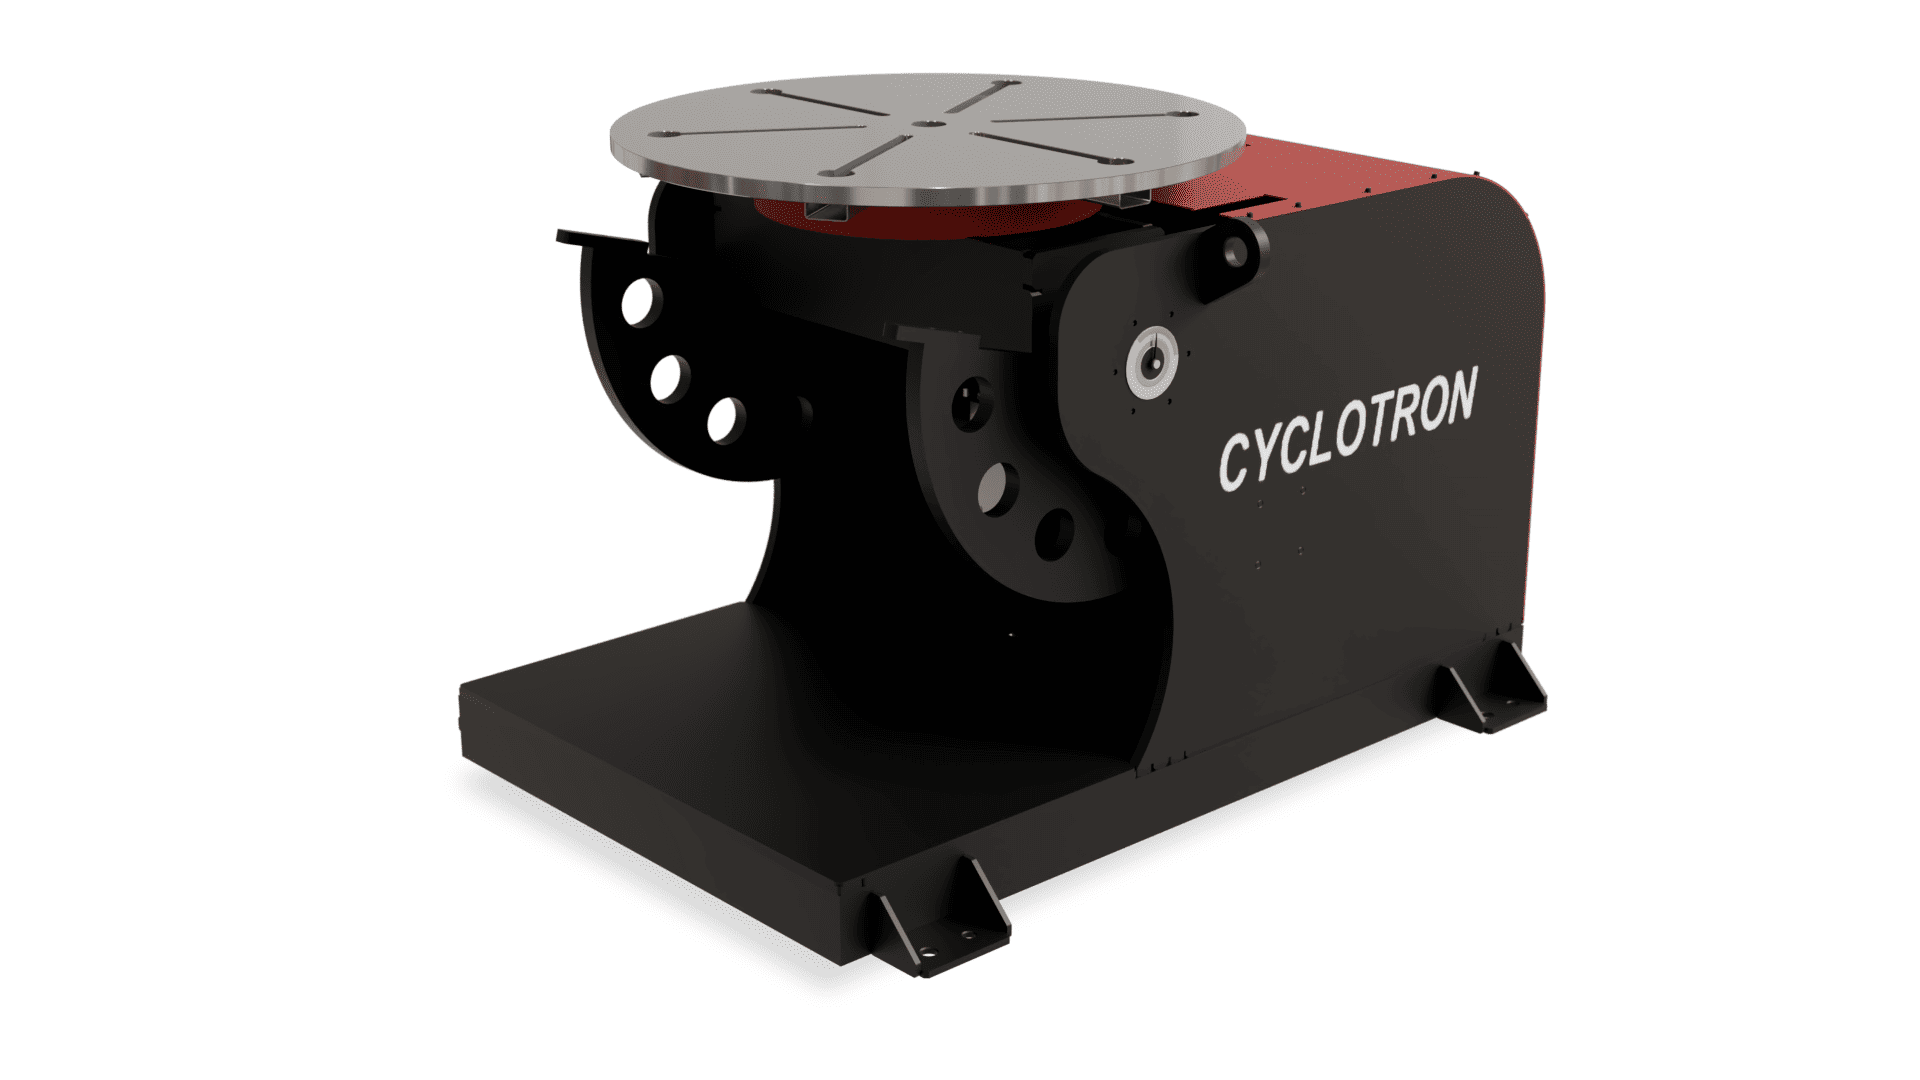
Universal welding positioner
SKU: CUP-2AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Tilting of face plate (0-135°)
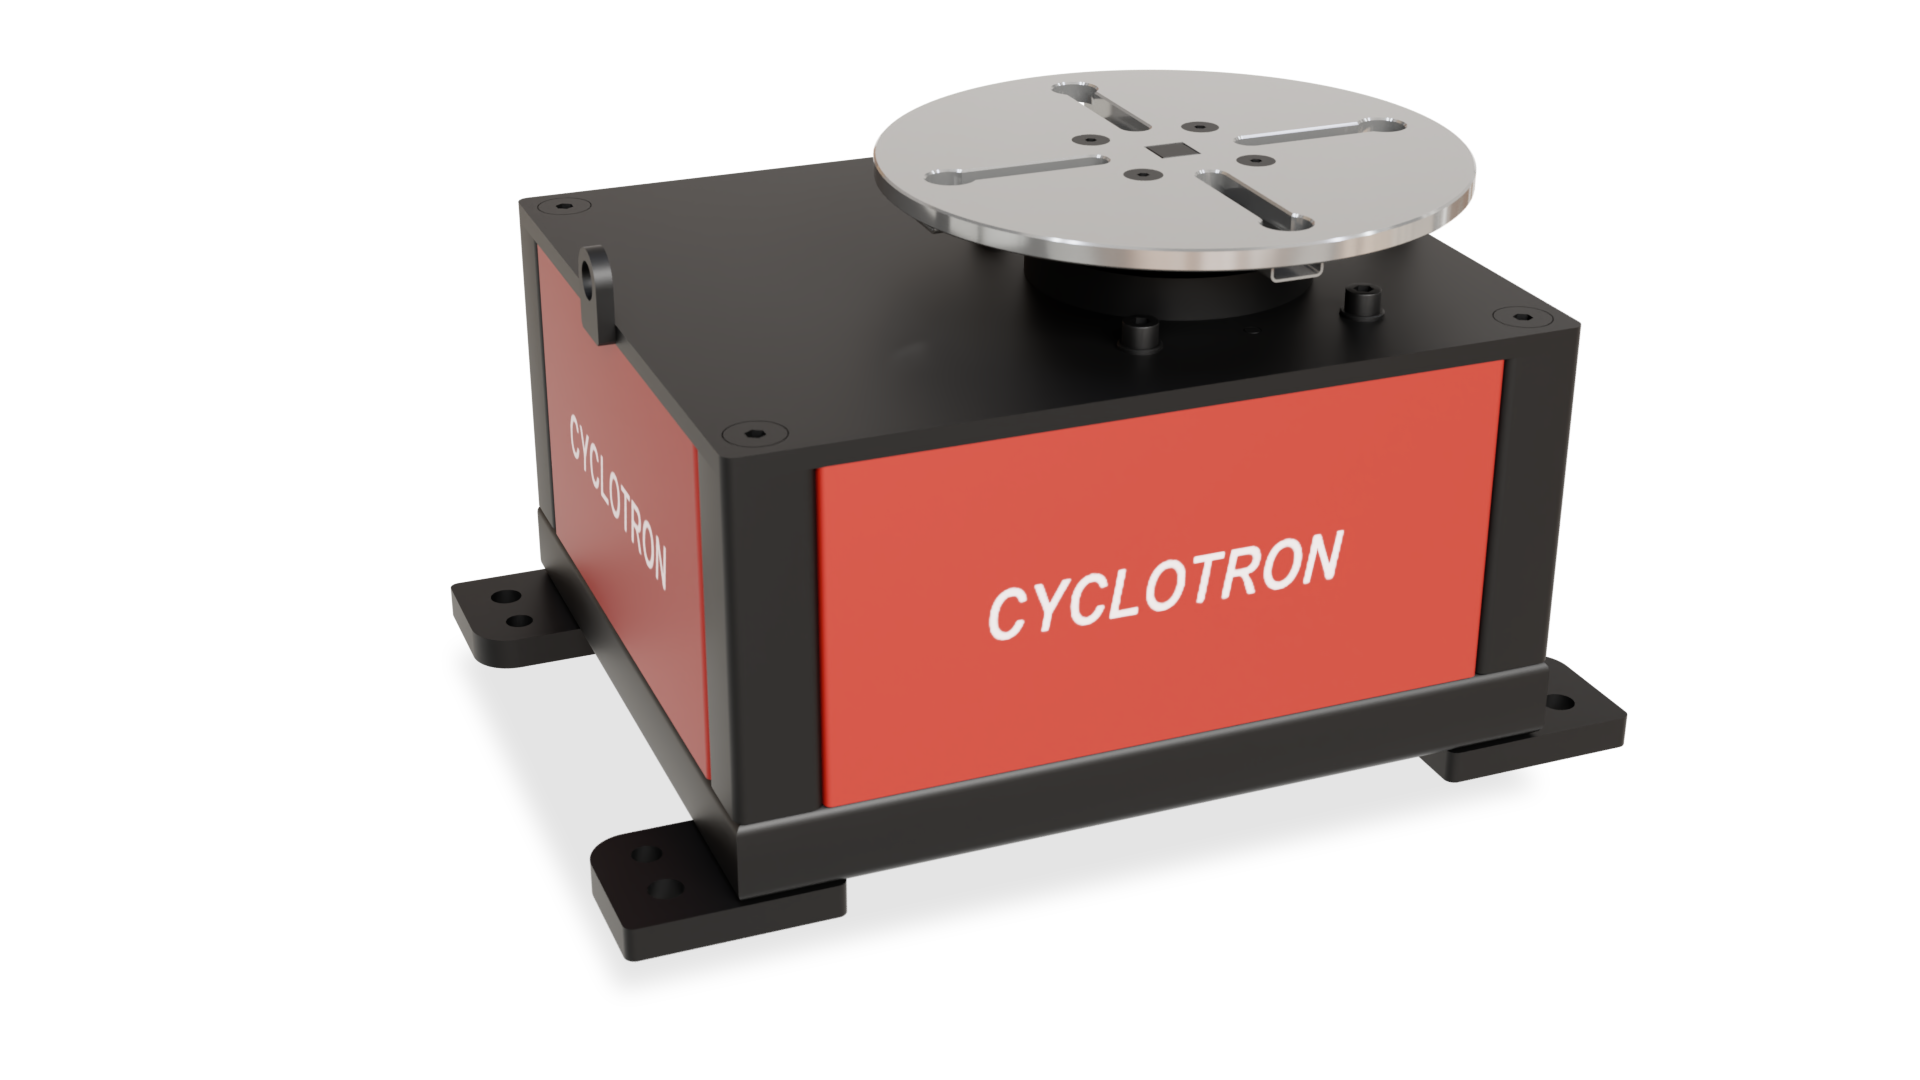
Mini Welding turntable
SKU: Mini-CTT-1AX
1st Axis: Face plate rotation (0-360°)
Headstock tailstock welding positioners in Chennai
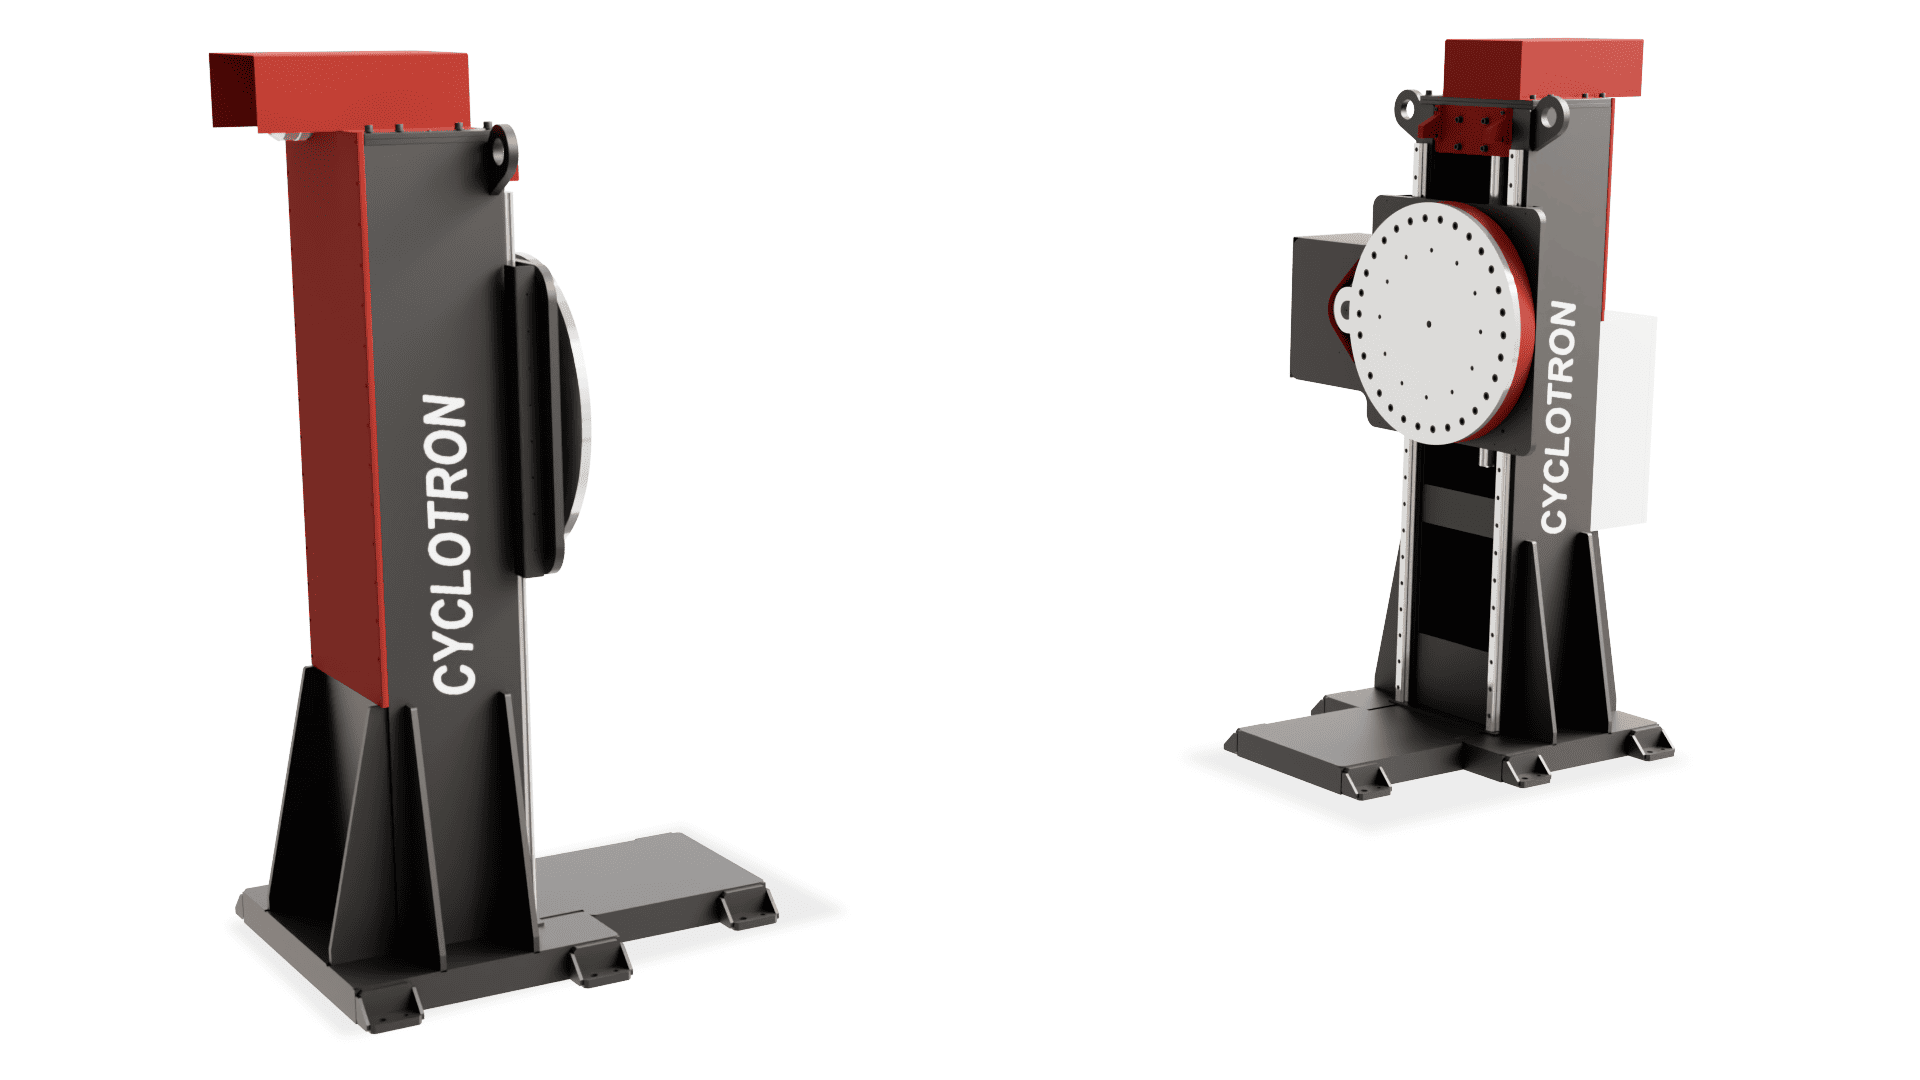
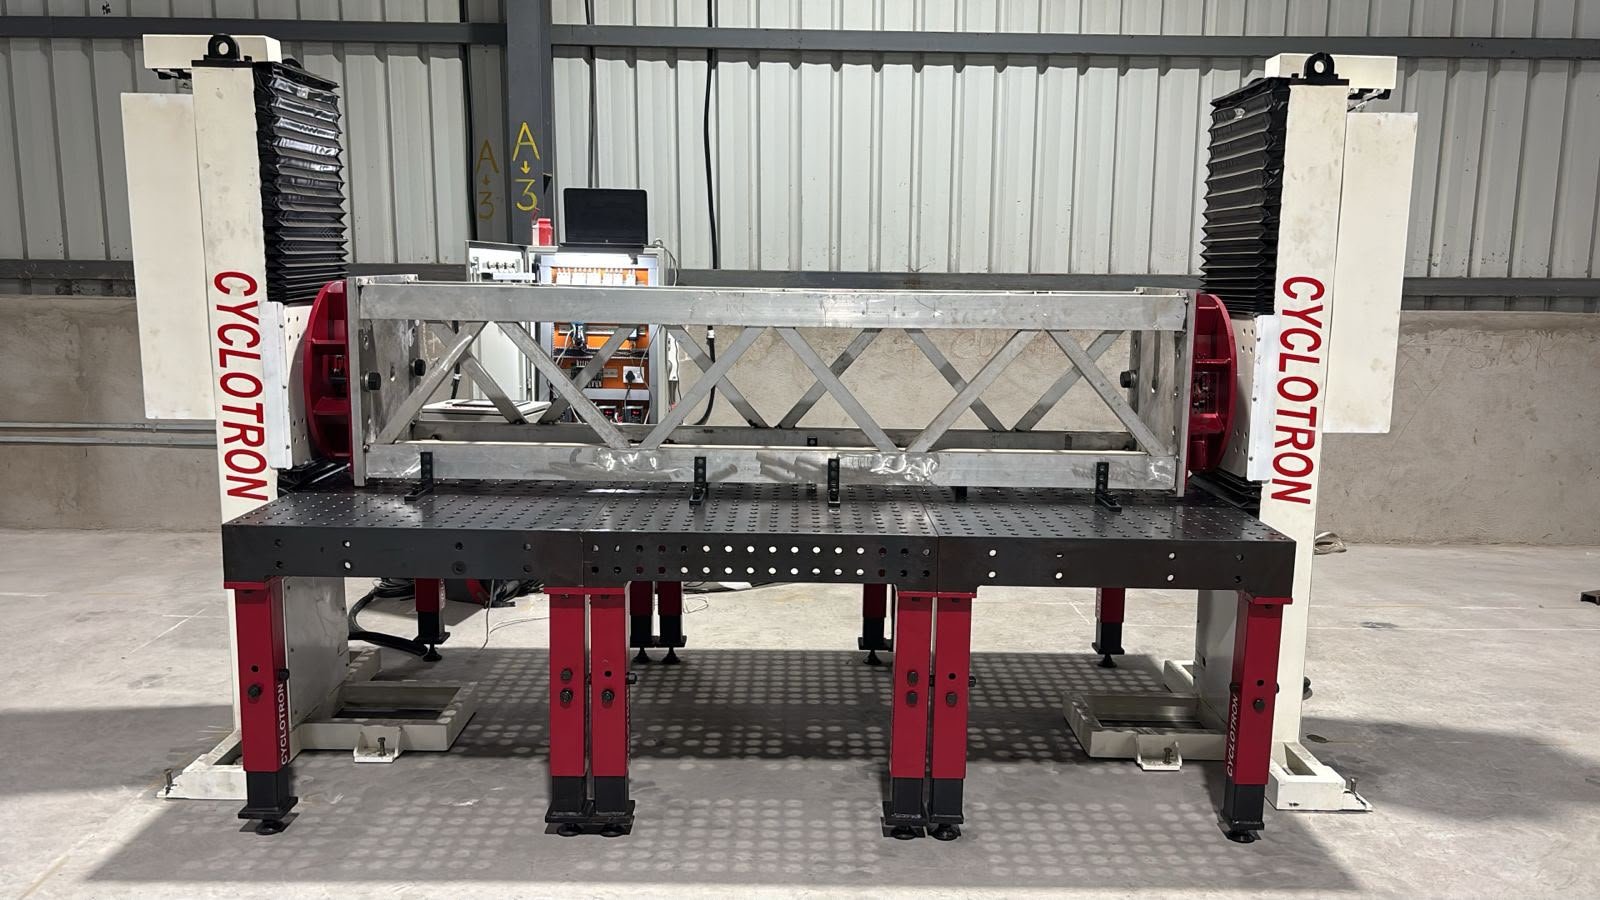
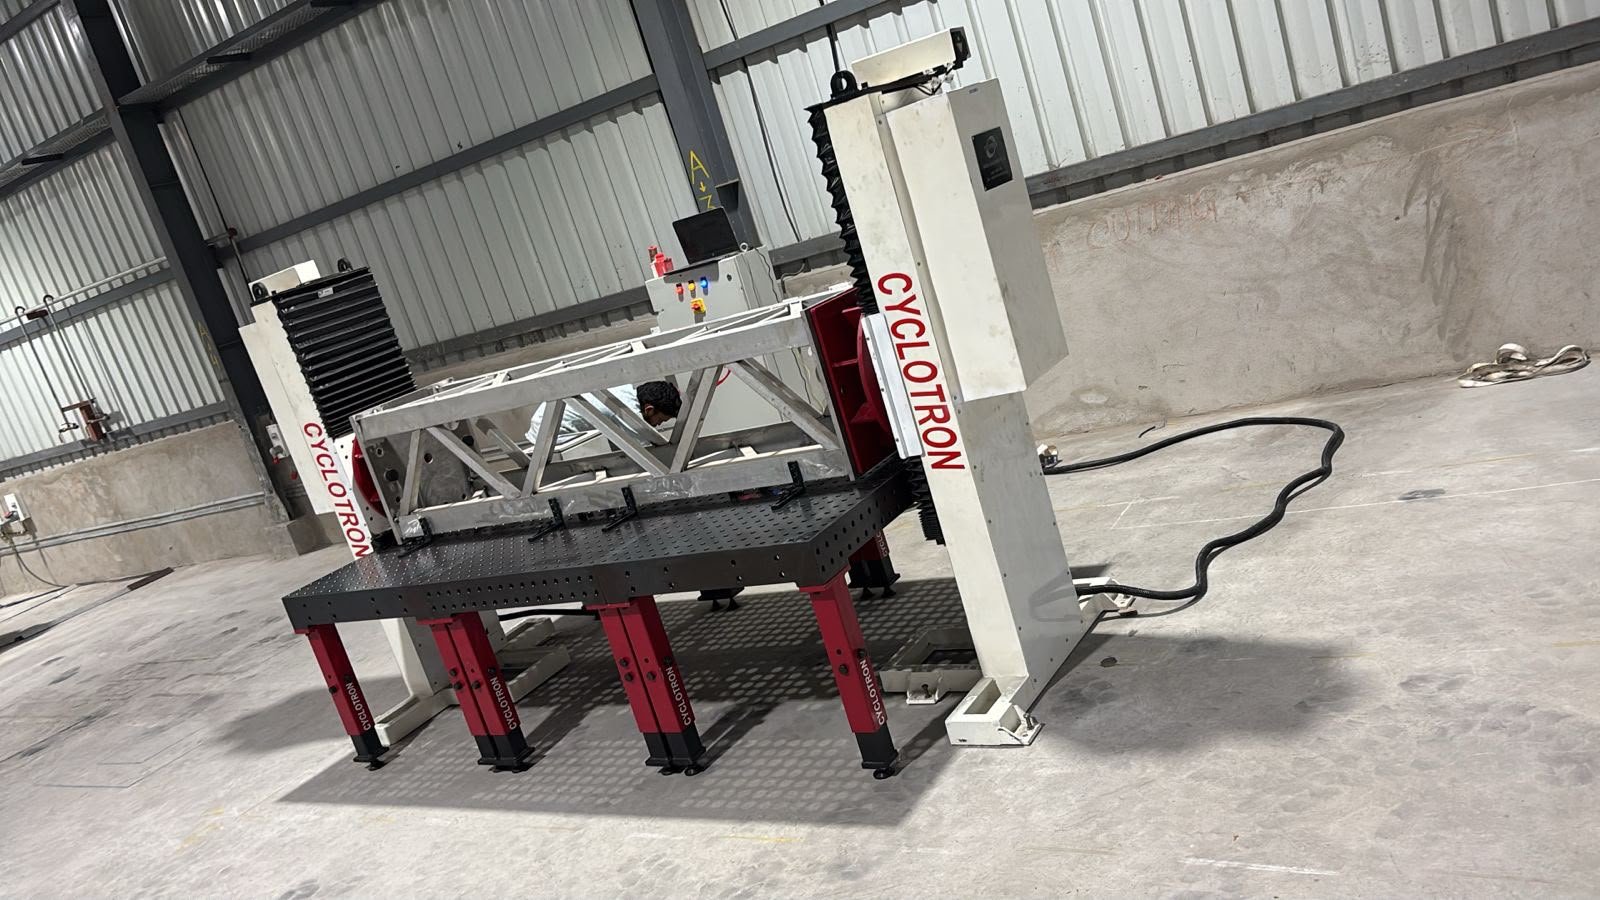
Headstock tailstock positioner-2 Axis
SKU: CY-HTP-2AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Height adjustment
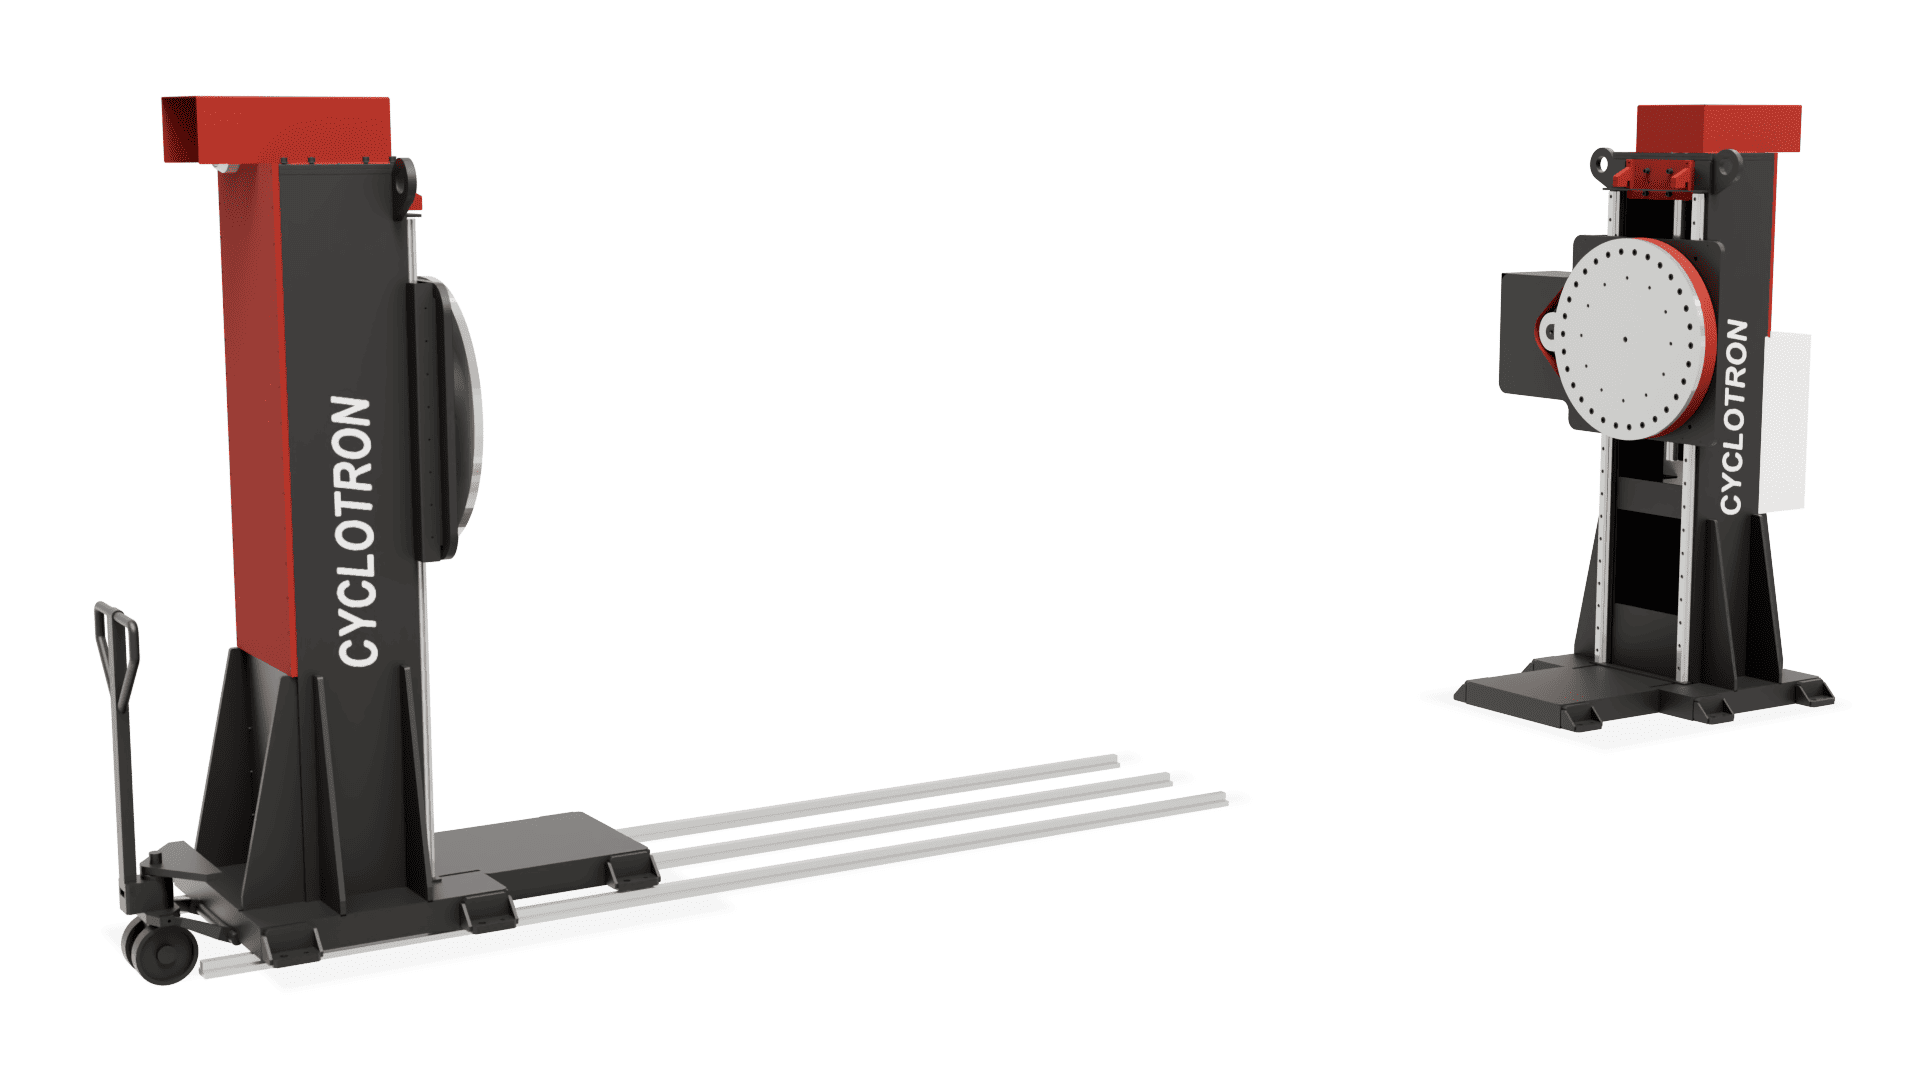
Headstock tailstock positioner-2 Axis with Rail
SKU: CY-HTP-2AX-R
1st Axis: Face plate rotation (0-360°)
2nd Axis: Height adjustment
Rail: Span between headstock and tailstock is adjustable
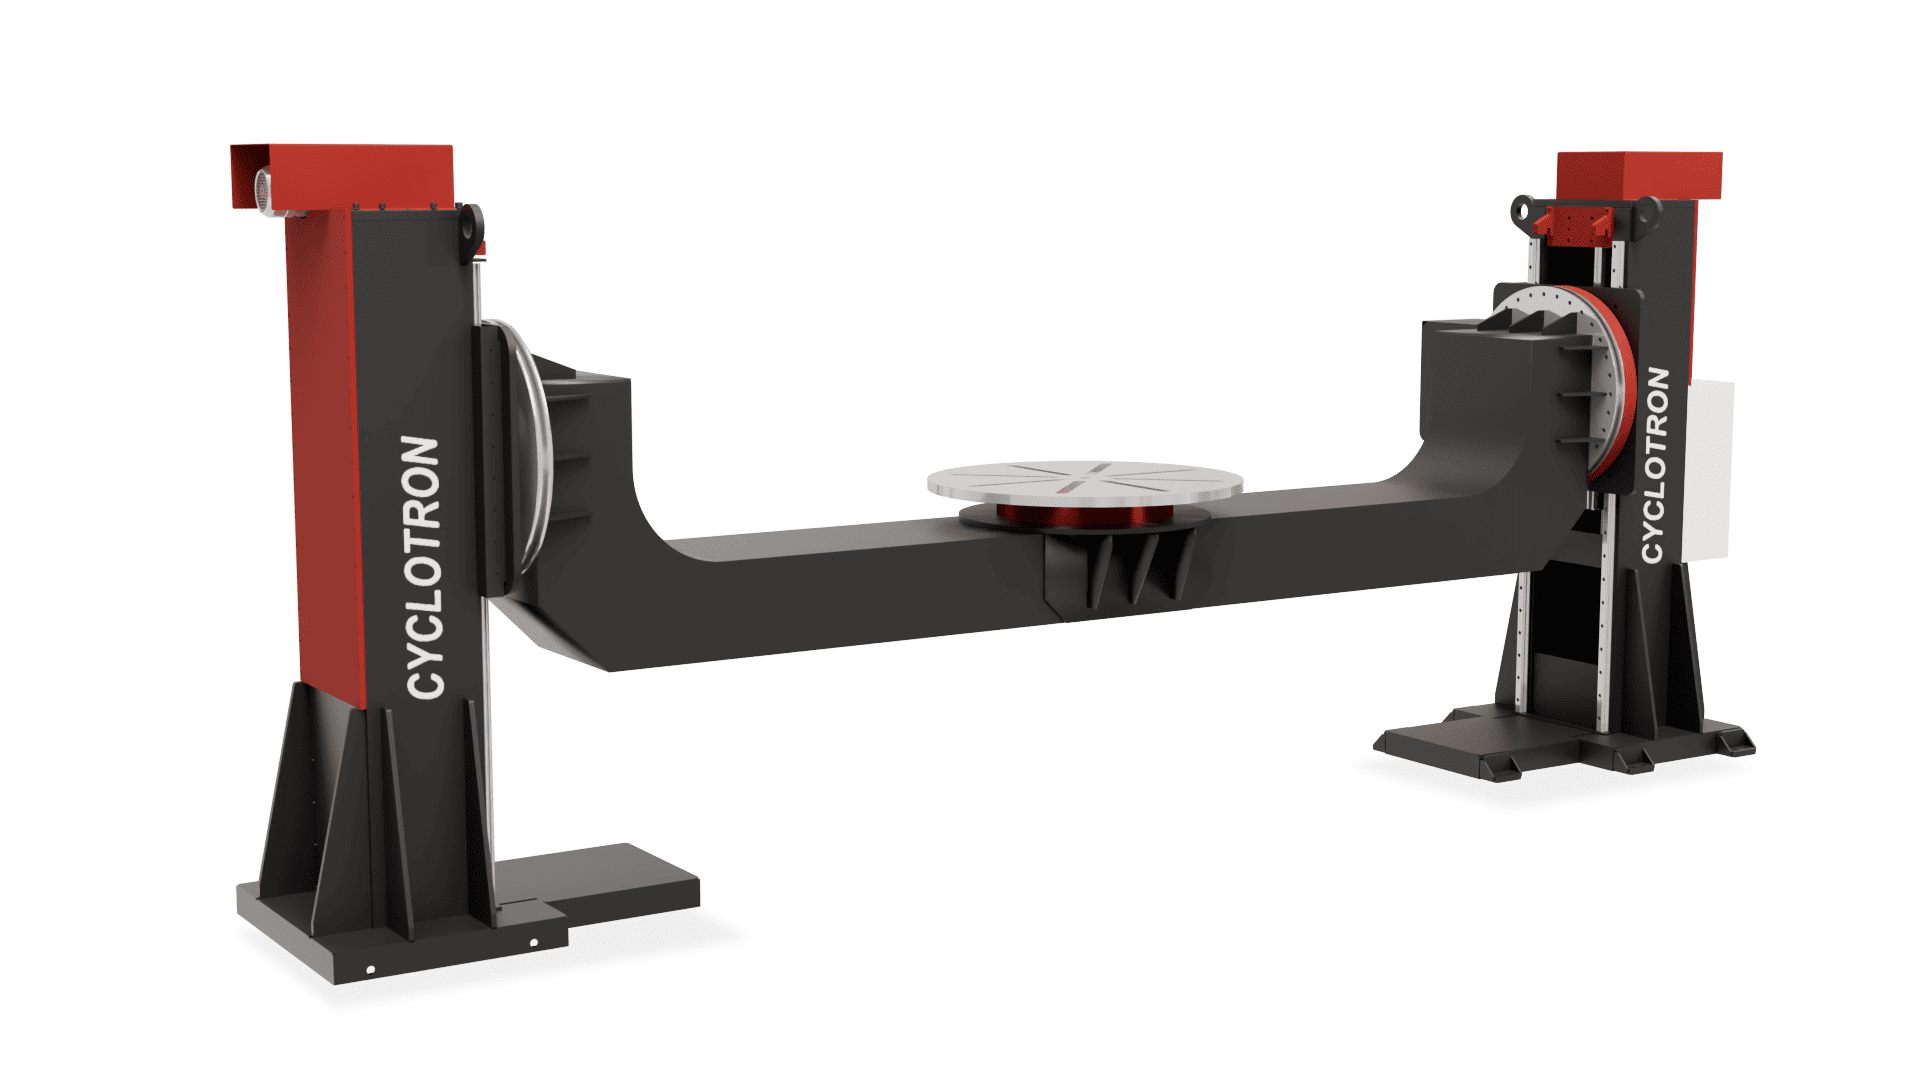
Headstock tailstock positioner-3 Axis
SKU: CY-HTP-3AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Tilting of the cradle (0-360°)
3rd Axis: Height adjustment
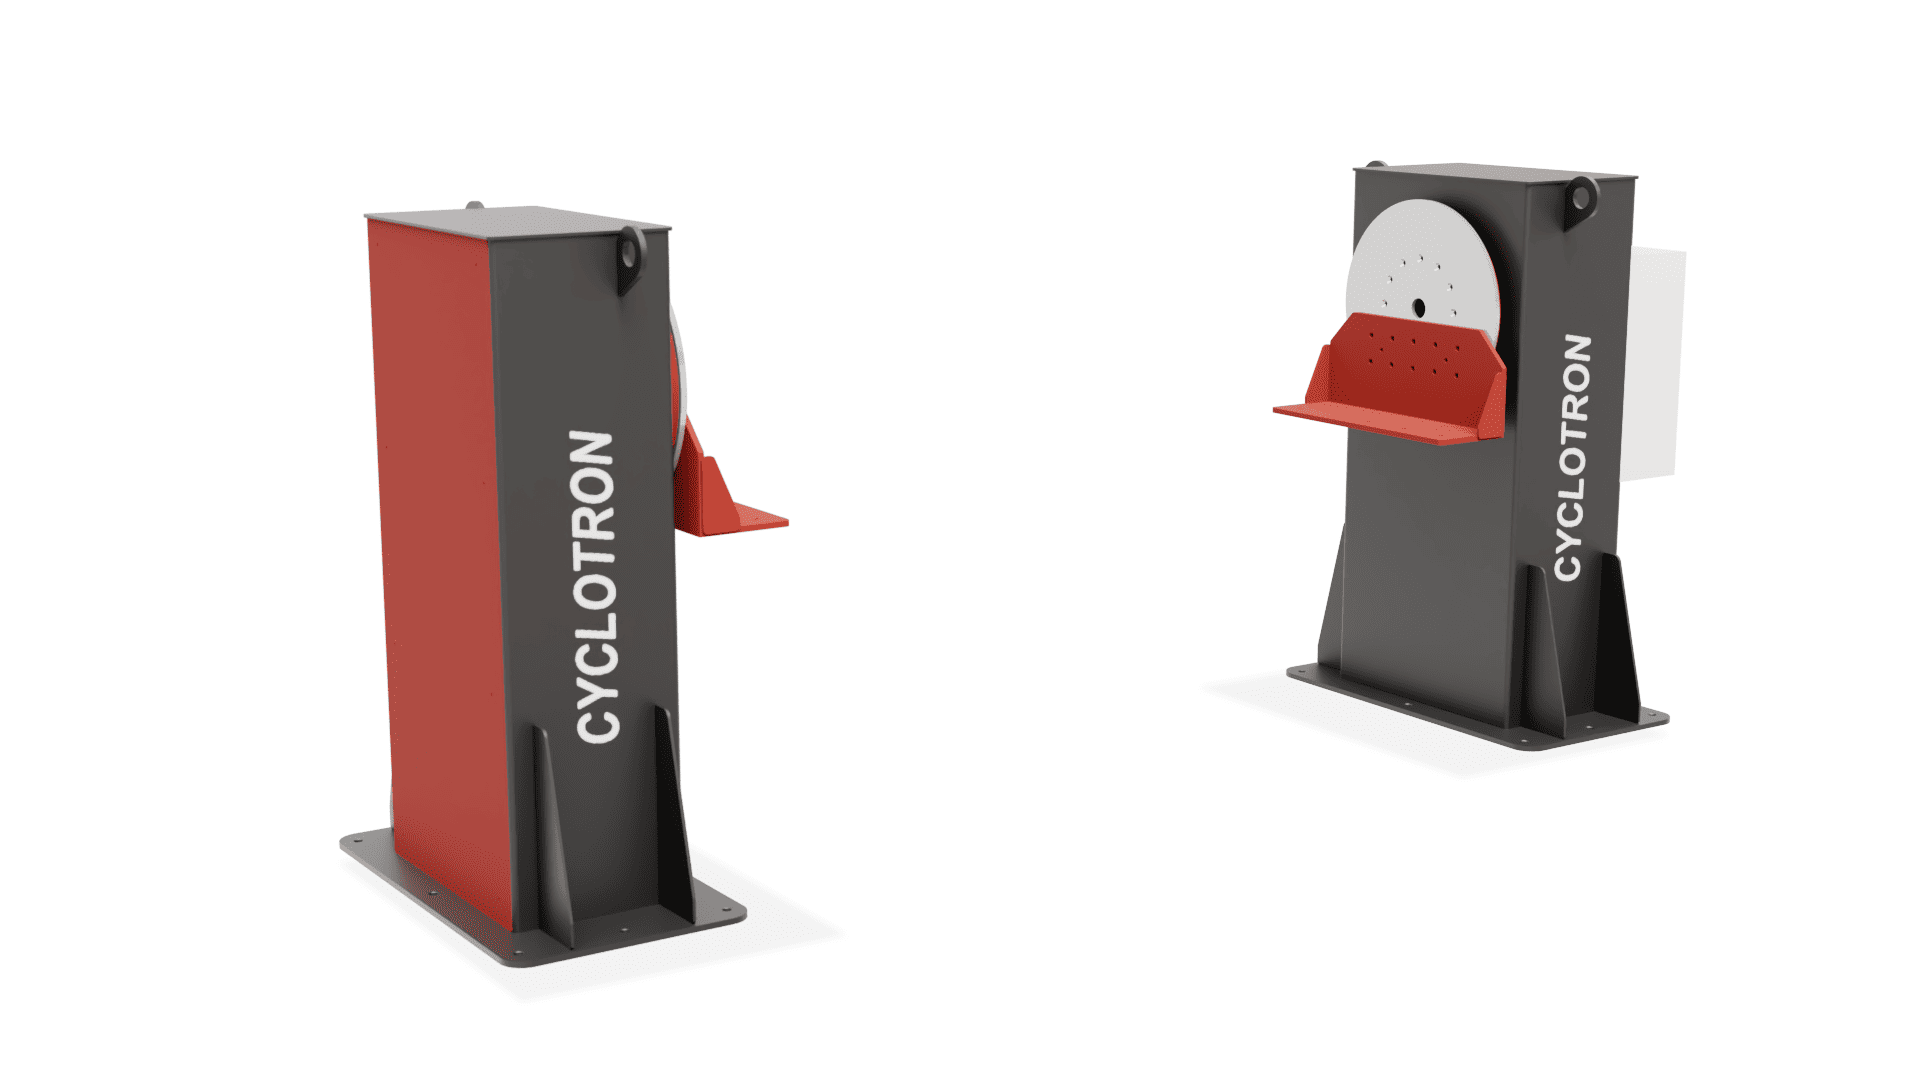
Headstock tailstock positioner-1 Axis
SKU: CY-HTP-1AX
1st Axis: Face plate rotation (0-360°)
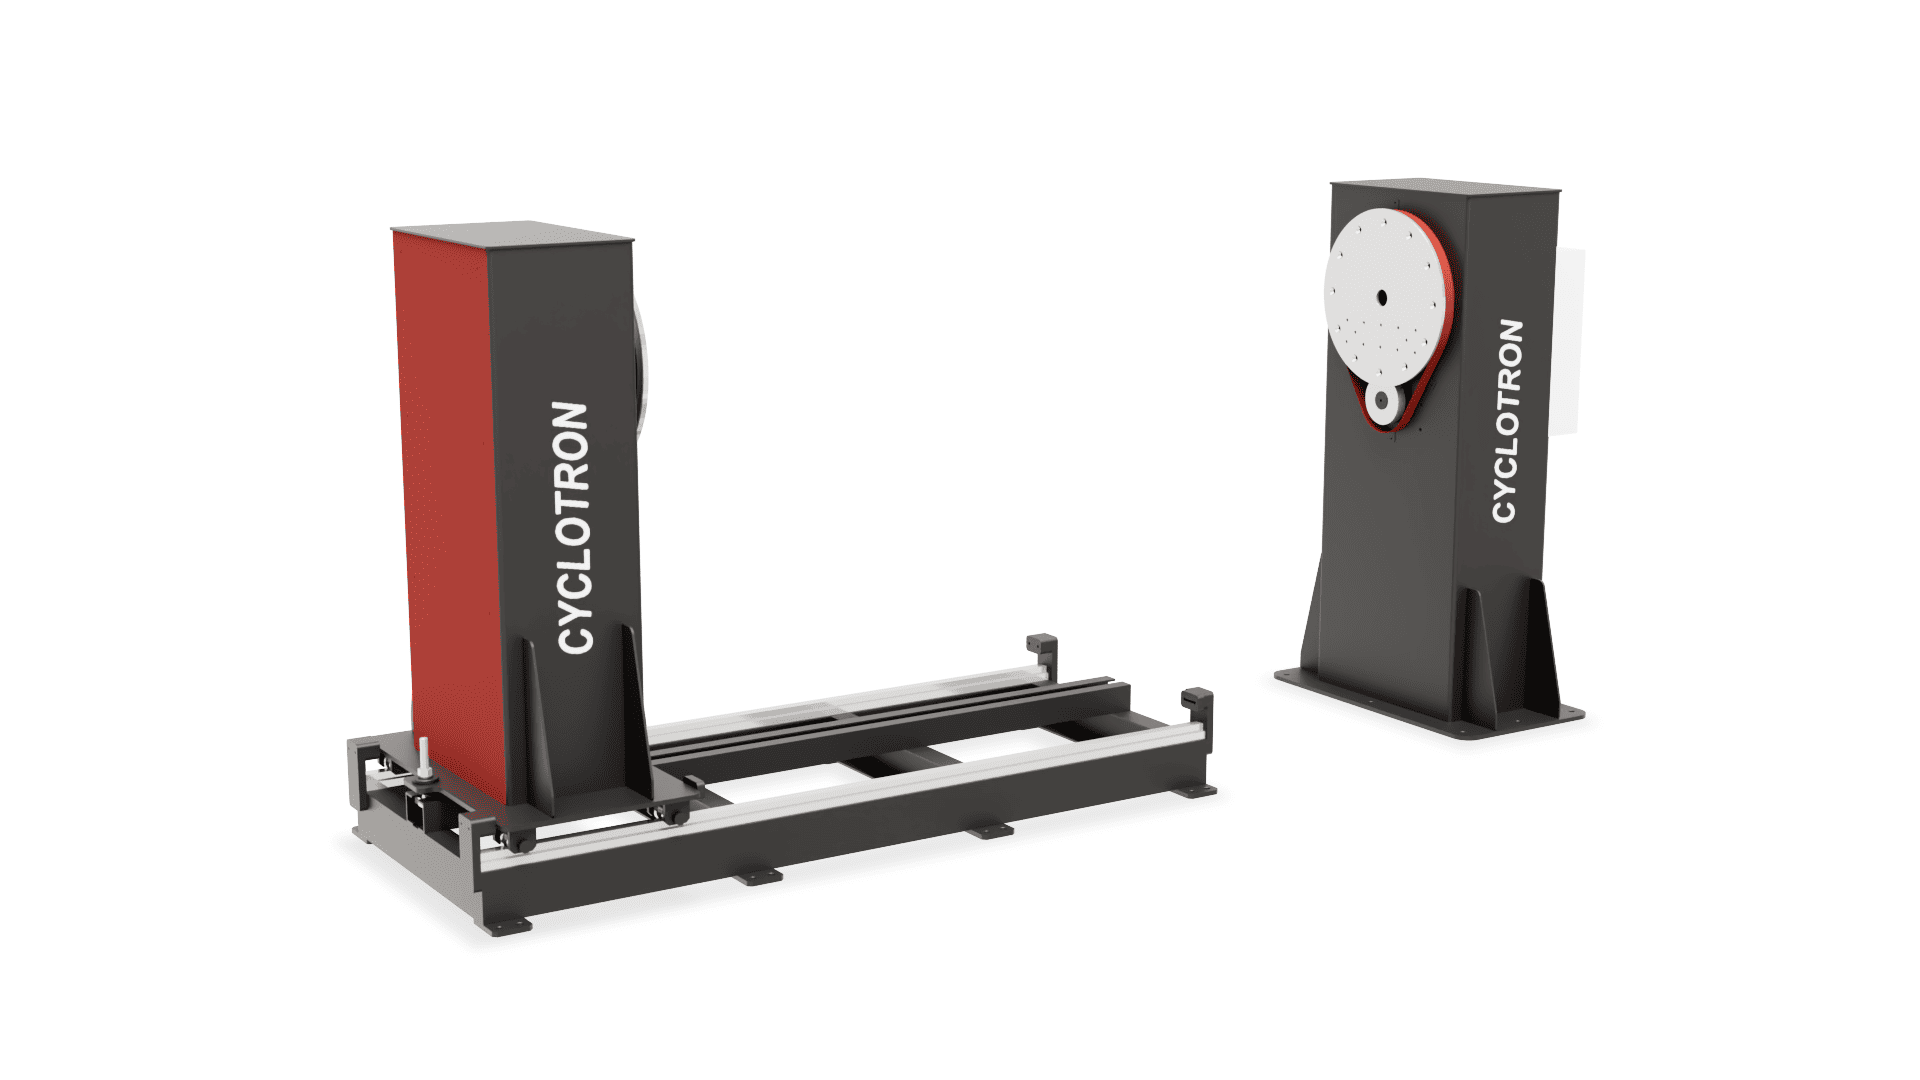
Headstock tailstock positioner-1 Axis with Rail
SKU: CY-HTP-1AX-R
1st Axis: Face plate rotation (0-360°)
Rail: Span between headstock and tailstock is adjustable
L type Welding Positioners in Chennai
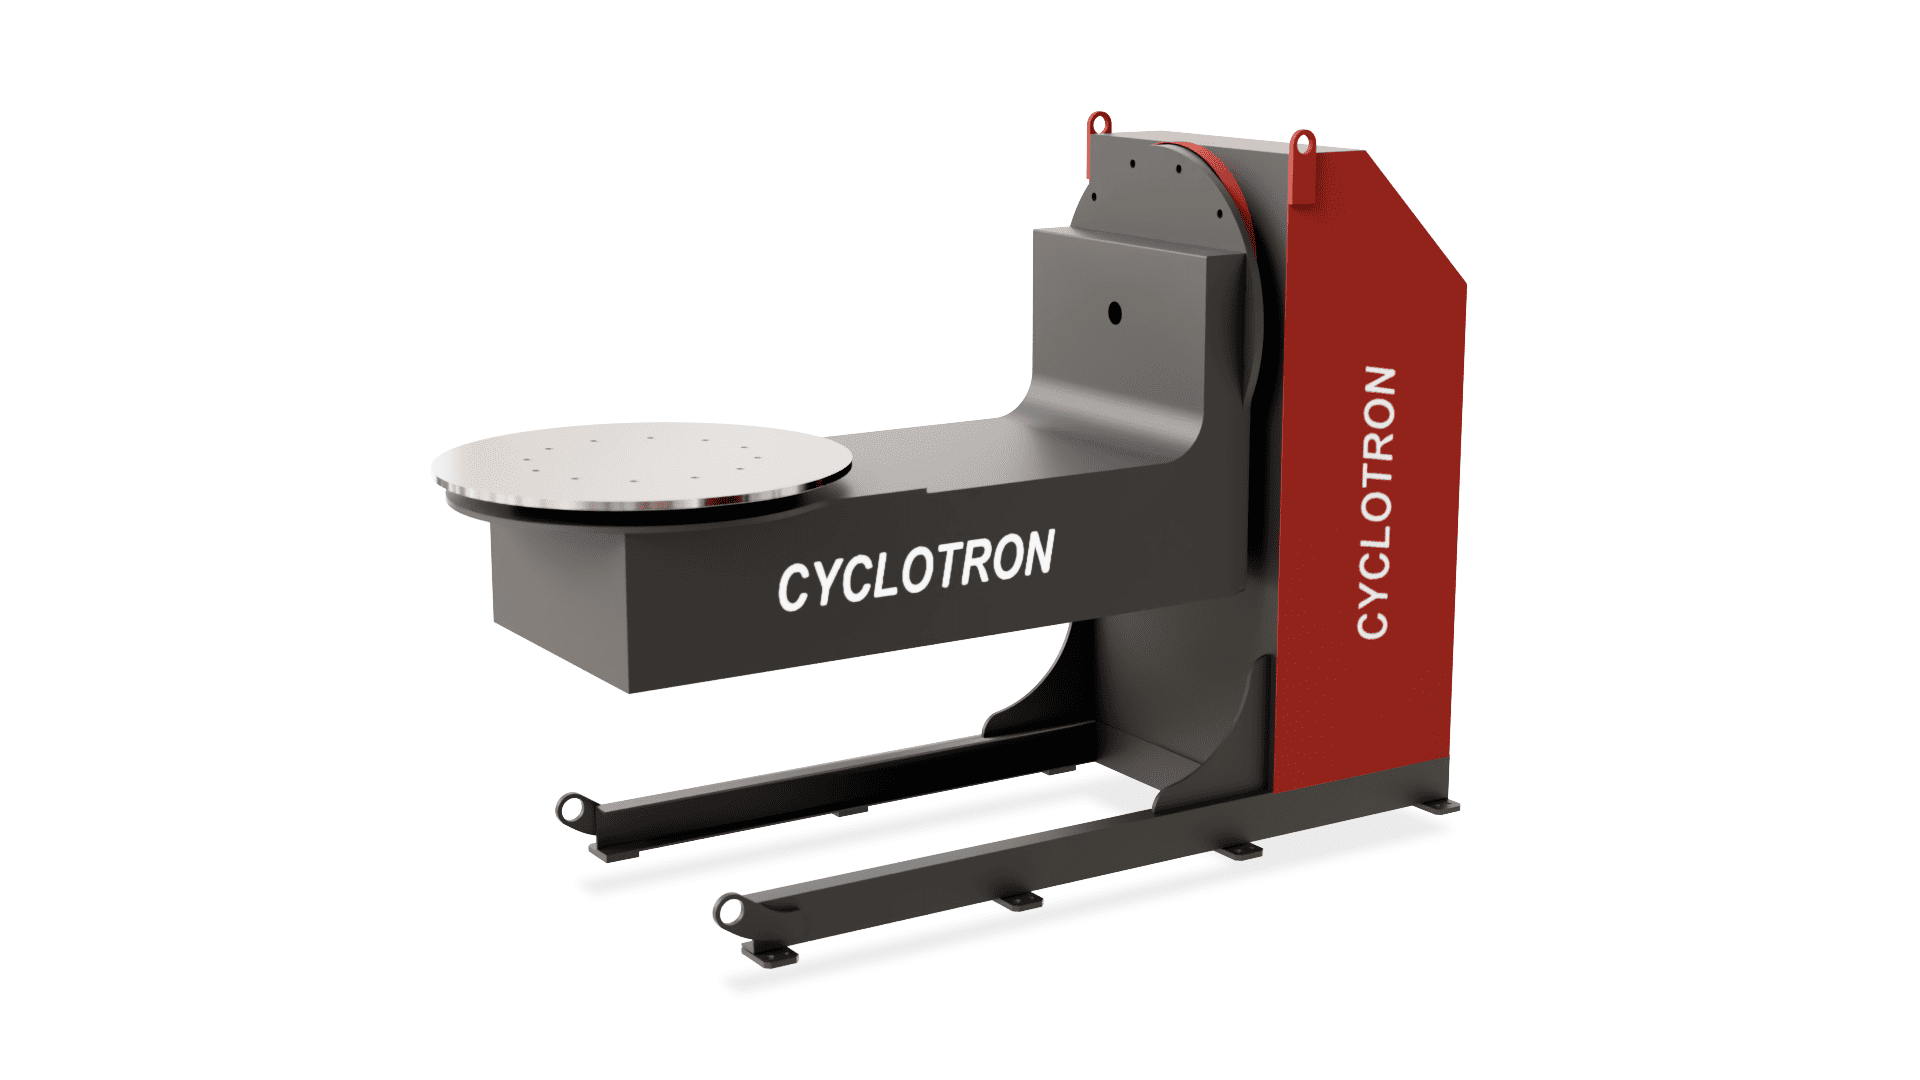
Cyclotron L Type Positioner 2AX
SKU: CLP-2AX
2 Axis (Rotation + Tilting)
Cycle time for using Welding Positioners in Chennai
The easiest way to understand the value of a positioner is to put your own production numbers into the equation.
Suppose an operator spends 5 minutes repositioning one component during welding. At 50 parts per shift:
5 minutes × 50 parts = 250 minutes per shift
That is more than 4 hours every shift spent on repositioning rather than productive welding.
Now suppose a positioner reduces that handling time to 1.5 minutes:
1.5 minutes × 50 parts = 75 minutes
You recover 175 minutes, or nearly 3 hours, per shift.
At 25 production days, that is approximately 73 hours of potential capacity recovered every month.
Your actual saving depends on your component, weld sequence and current handling process.
For higher-volume lines, a two-station configuration can improve utilisation further. One component can be welded while the operator loads or unloads the second station. The welder or robot does not have to sit idle while the next component is prepared.
That changes the buying case completely. You are not simply purchasing equipment to rotate a component. You are investing in more productive minutes per shift.
Long Parts: Chassis, Frames and Underframes in Chennai
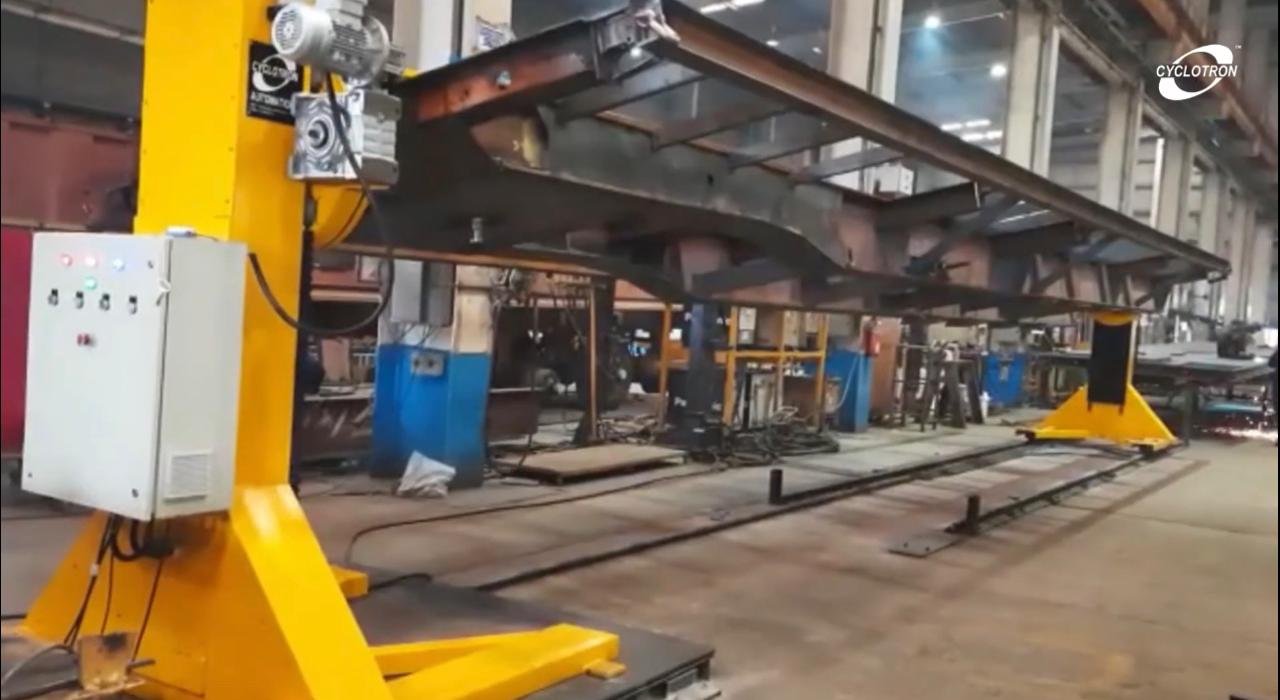
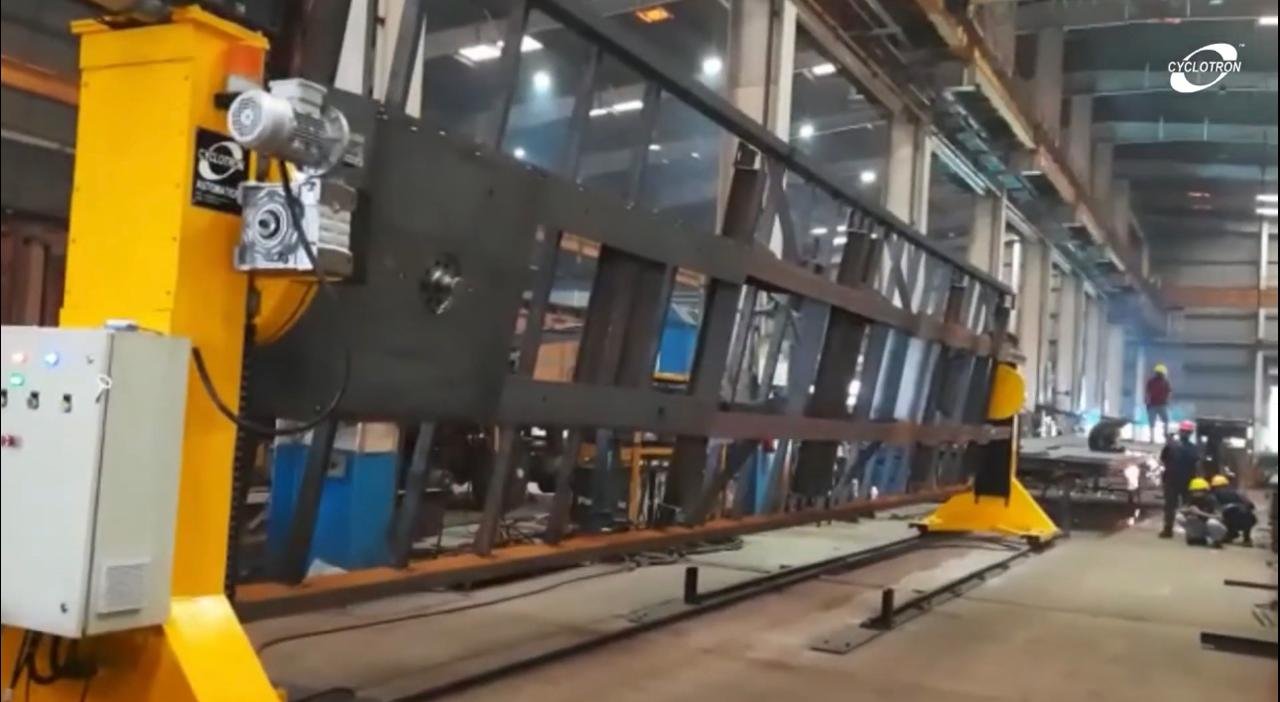
Long components create another positioning challenge. Supporting a large chassis or railway underframe at only one end can make loading, rotation and welding difficult.
A headstock-tailstock positioner supports the component at both ends and allows it to rotate as an assembly. For changing component lengths, an adjustable rail lets the tailstock move to the required position.
This configuration is particularly relevant for commercial vehicle chassis, railway coach structures, bogies, underframes and long fabricated frames.
Instead of manually moving or repeatedly repositioning a long structure, the operator can rotate the component into the required welding position.
The machine must be specified around the maximum span, component weight, centre of gravity and loading arrangement.
Using Welding Positioners for Chennai's Fabrication Clusters
Chennai’s manufacturing belt combines some of India’s largest automotive operations with railway and heavy engineering fabrication.
Oragadam and Sriperumbudur have a strong automotive OEM and supplier base, producing vehicle frames, chassis components, brackets, exhaust assemblies and welded sub-assemblies.
Ambattur supports engineering and automotive component manufacturers working with machine frames, housings, fabricated structures and industrial components.
Irungattukottai adds automotive and industrial fabrication, while Gummidipoondi and Thiruvallur support heavier engineering and fabrication requirements.
In Manali, process and heavy engineering applications can involve larger fabricated structures and industrial equipment.
What Chennai Fabrication units orders the most
Chennai’s production environment puts a premium on throughput and repeatability.
Headstock-tailstock systems are particularly suited to long chassis, underframes, and railway structures. Robotic-ready positioners are relevant where the machine forms part of an automated welding cell.
For repetitive production, configuration matters because the objective is to minimise loading time, repositioning time, and operator waiting.
A higher-capacity machine is not automatically the better investment. The better machine is the one that gives your production line more usable welding time per shift.
Delivery and Service for Welding Positioners in Chennai
We manufacture our welding positioners at our Pune plant and supply them to customers across Chennai and Tamil Nadu.
Transit from Pune: 24-48 hours by road
Before dispatch, we review the installation area, unloading arrangement, electrical requirements and commissioning plan. Our engineers can support installation, commissioning and operator training as agreed for the project.
Tamil Nadu service coverage: Our local site and support engineers
FAQs
How much cycle time does a positioner actually save per part?
It depends on your current handling process. If repositioning takes 5 minutes per part and you produce 50 parts per shift, that is 250 minutes of handling time. Reducing it to 1.5 minutes saves 175 minutes per shift. We can calculate the potential saving using your actual production data.
What is the maximum part length a headstock-tailstock can handle?
That depends on the positioner and rail configuration. Our Cyclotron headstock-tailstock positioners can handle 20 mtrs part length. We also consider component weight, centre of gravity and support requirements before recommending a configuration.
Can you supply CE-documented machines for export fabricators?
Where applicable, we can discuss CE documentation and project-specific requirements before manufacturing. Share your export destination and customer specifications during quotation
Do you support two-station load-while-welding setups?
Yes, where the selected configuration supports two-station operation. This allows one component to be loaded or unloaded while another is being welded, reducing waiting time and improving cell utilisation