Welding Positioner in Hosur
Cyclotron Manufactures the Best Welding Positioner in Hosur, Karnataka. We serve the region and have customers from SIPCOT Phase I and II, Zuzuvadi, Mathigiri, and Bagalur region
We are manufacturers, not resellers. That means you can speak directly with the team that builds your machine, understand its capabilities and see it working before you make a purchase.
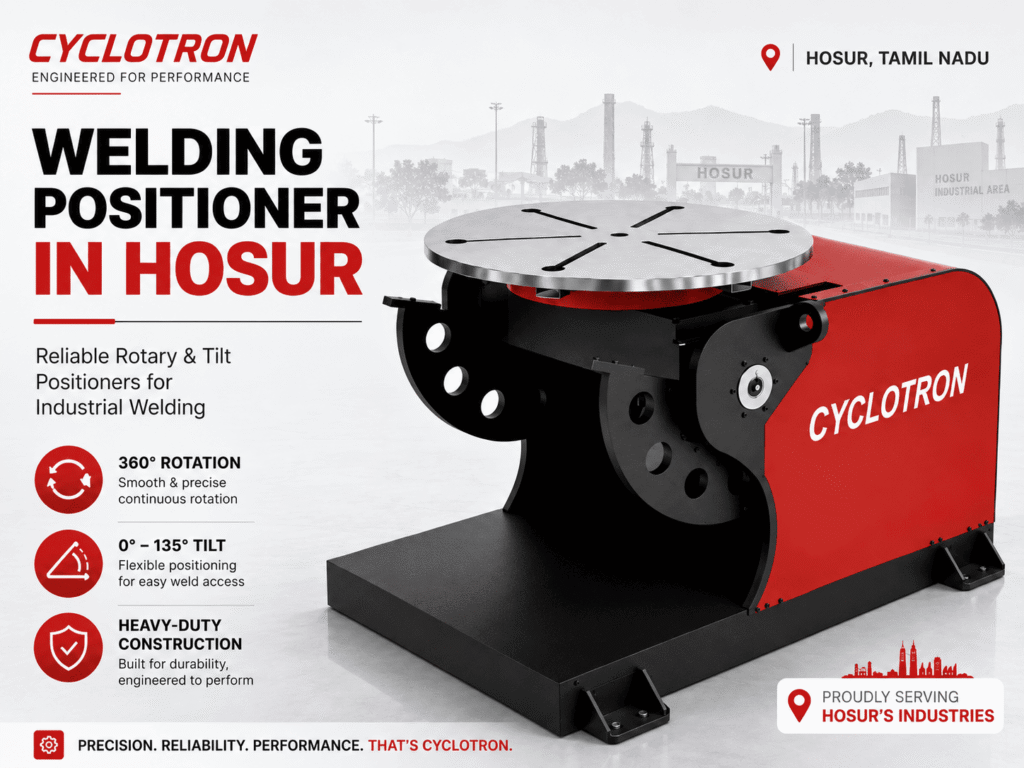
Welding positioner manufacturer in Hosur
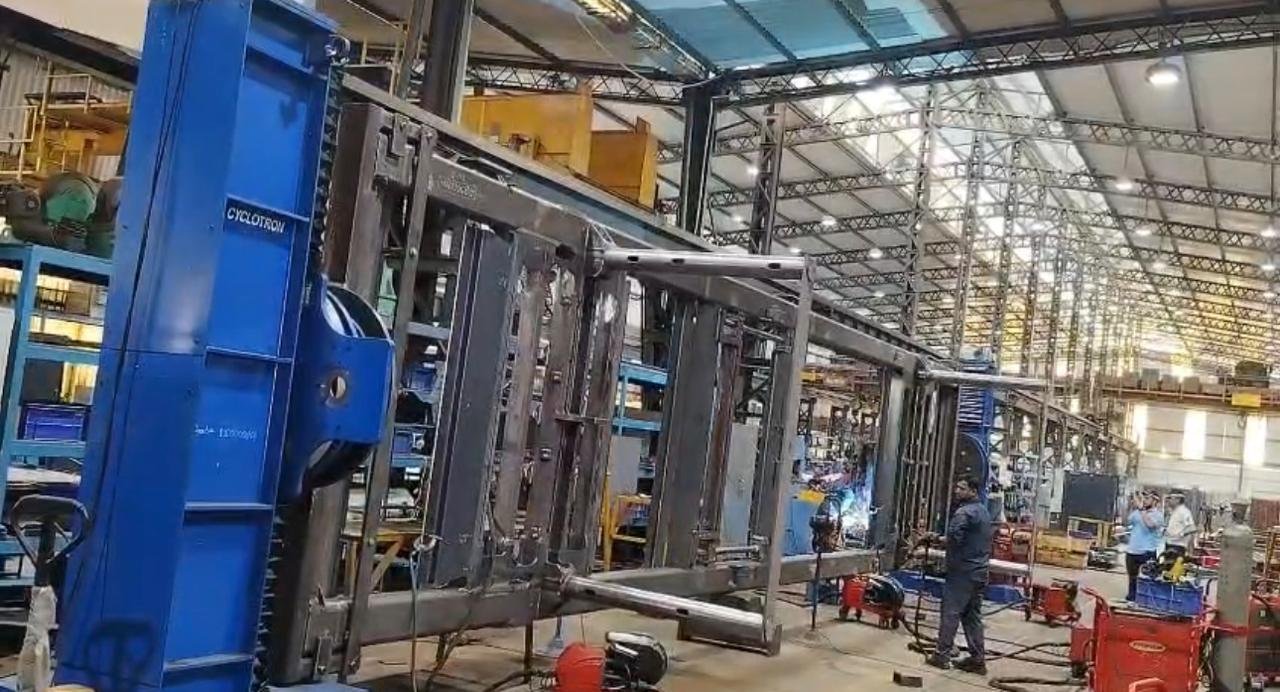
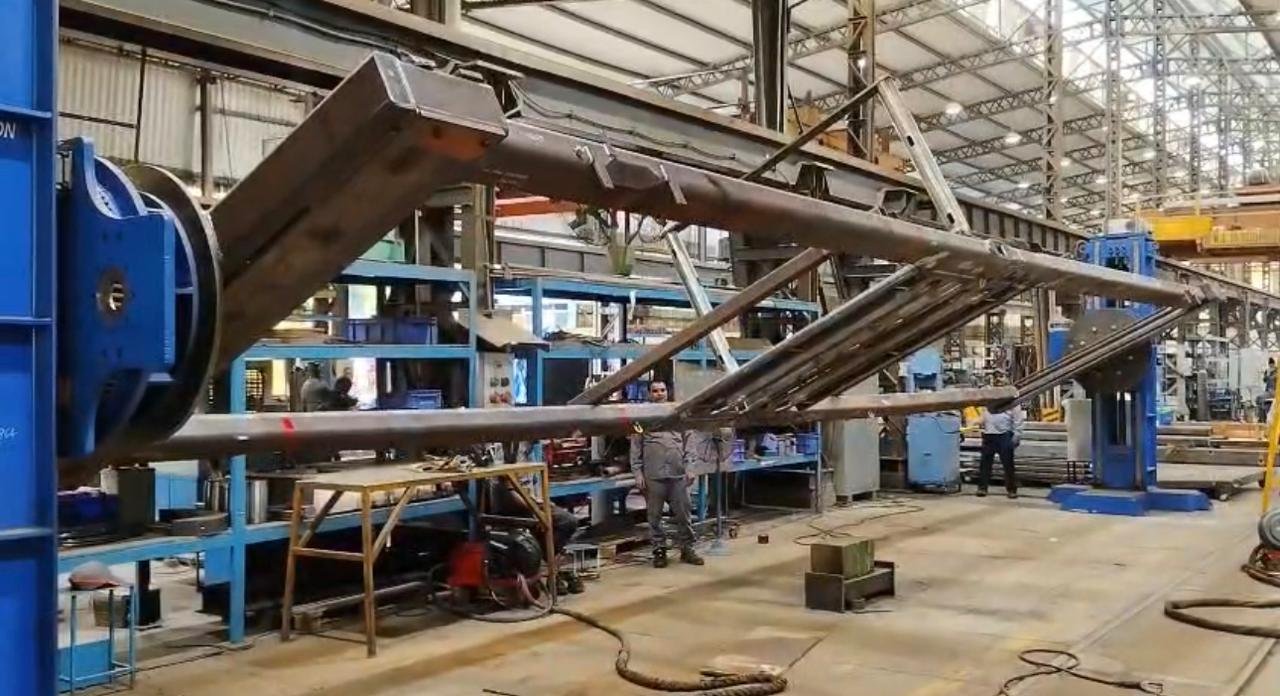
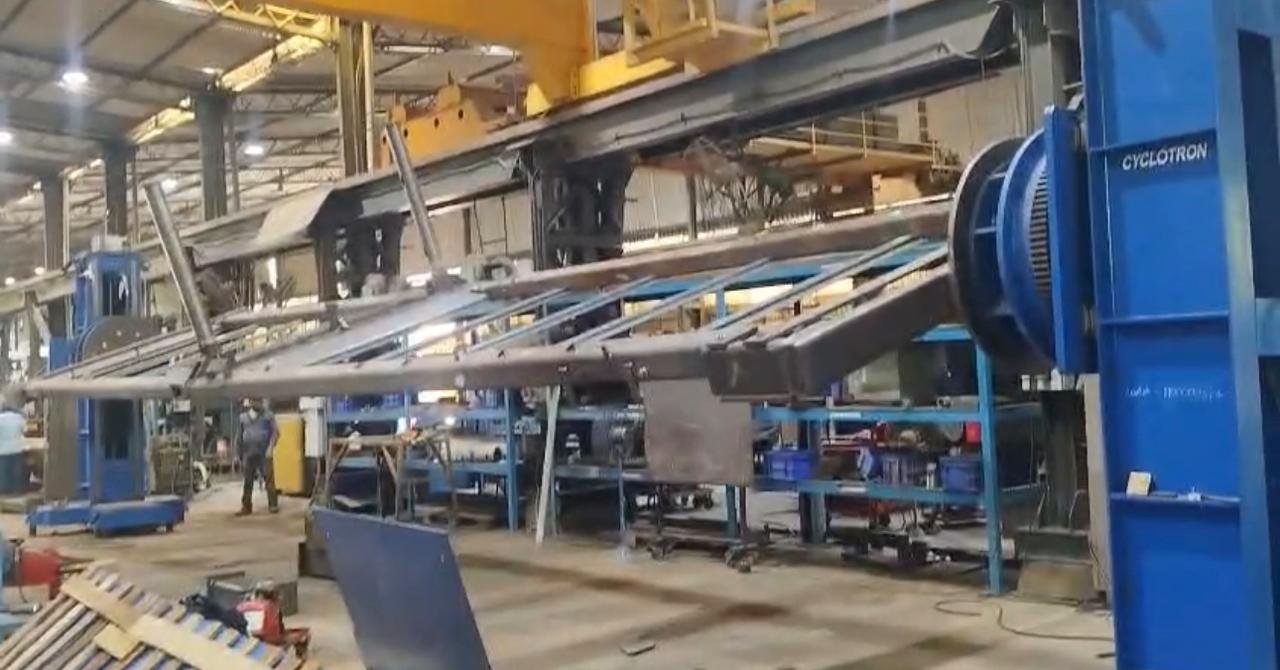
Cyclotron manufactures industrial welding positioners from 100 kg to 100 Tons capacity, designed for robotic/manual welding, heavy fabrication, and high-production welding environments.
500+
Successfully Project Finished.
7+
Years of experience with proud
100+
Companies worldwide
50+
Colleagues & counting more daily
Welding positioner manufacturer in Hosur
Hosur’s fabrication requirements are changing with the growth of EV and two-wheeler component manufacturing. For aluminium and thin-gauge components, the welding positioner needs to provide controlled movement without compromising the welding process.
We supply welding positioners across SIPCOT Phase I and II, Zuzuvadi, Mathigiri, and Bagalur. Hosur is approximately 40 km from Bangalore, and both locations are covered through the same engineering service network.
Whether you are welding battery enclosures, brackets, frames, or smaller two-wheeler components, we can help specify the positioner around your material, component geometry, welding process, and required rotation control.
Trusted By Industry Leaders from Hosur
Rotary welding positioner in Hosur
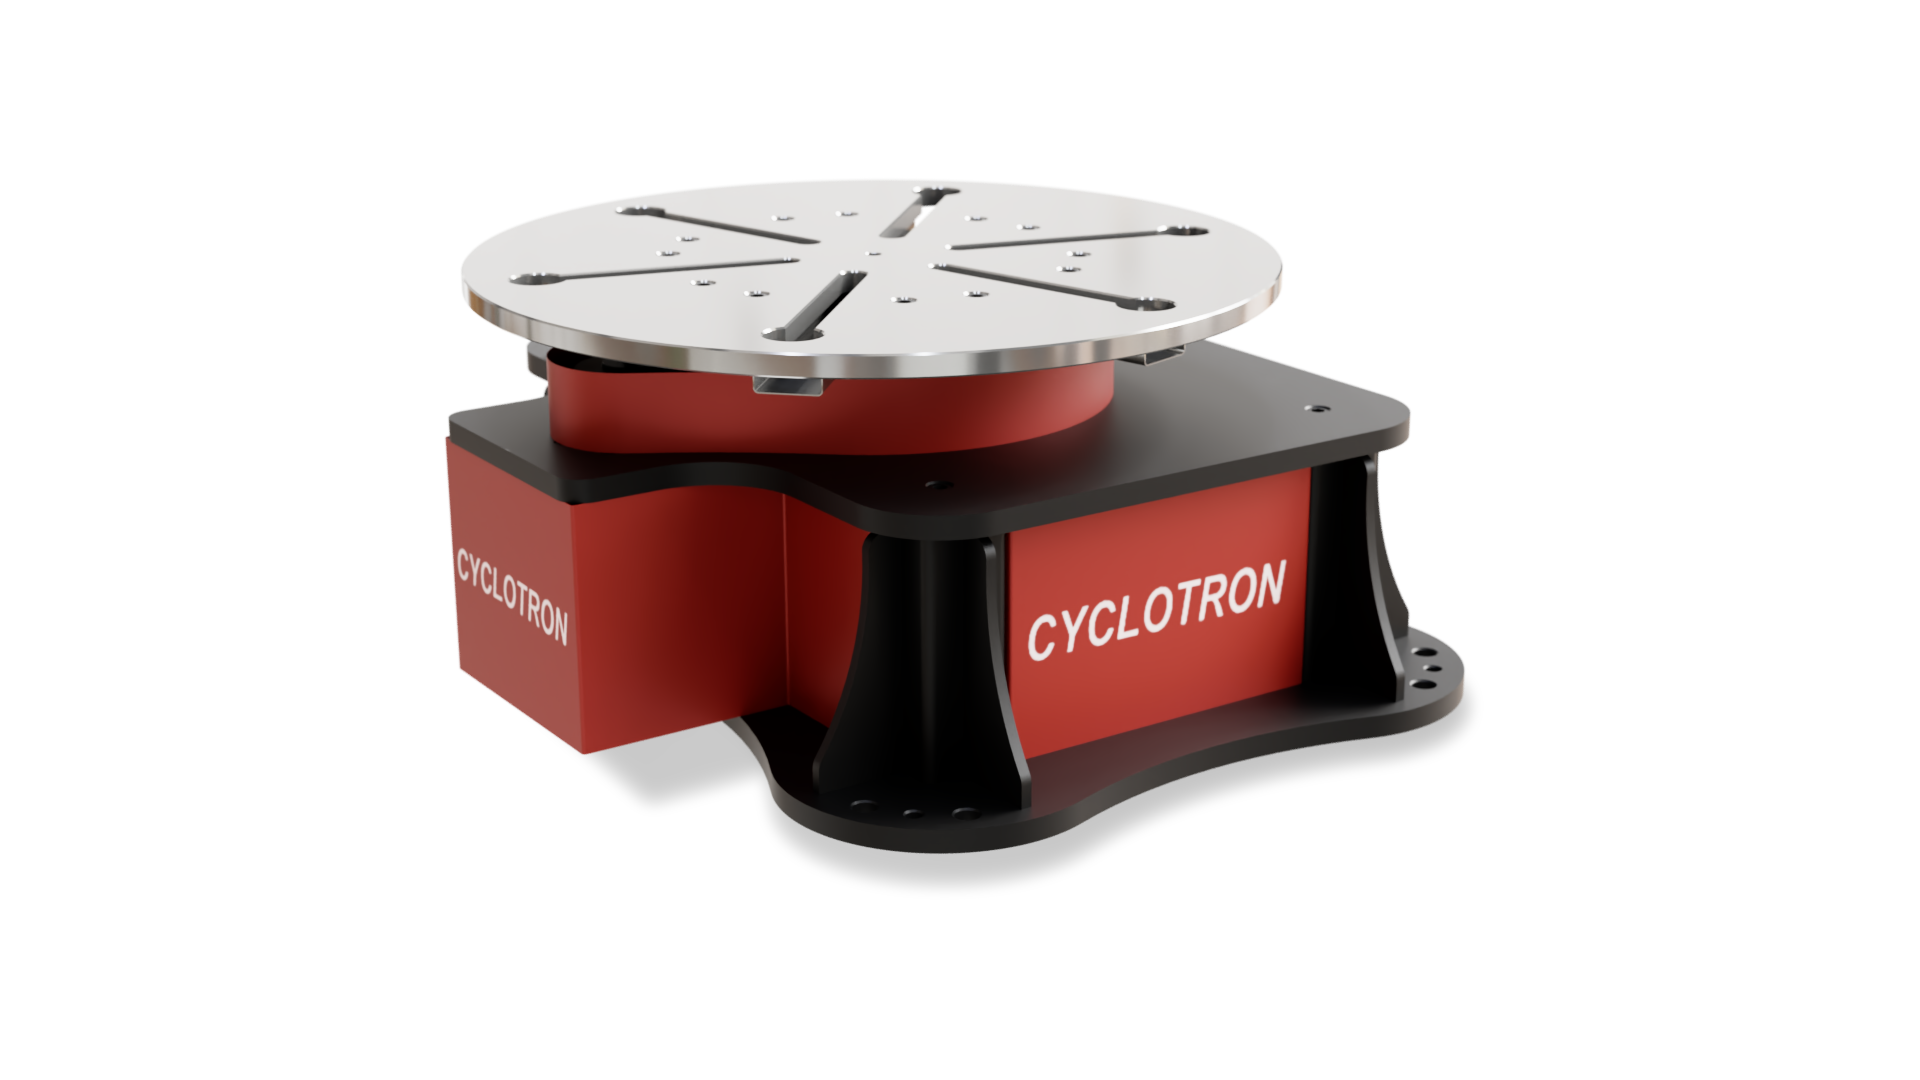
Welding turntable
SKU: CTT-1AX
1st Axis: Face plate Rotation (0-360°)
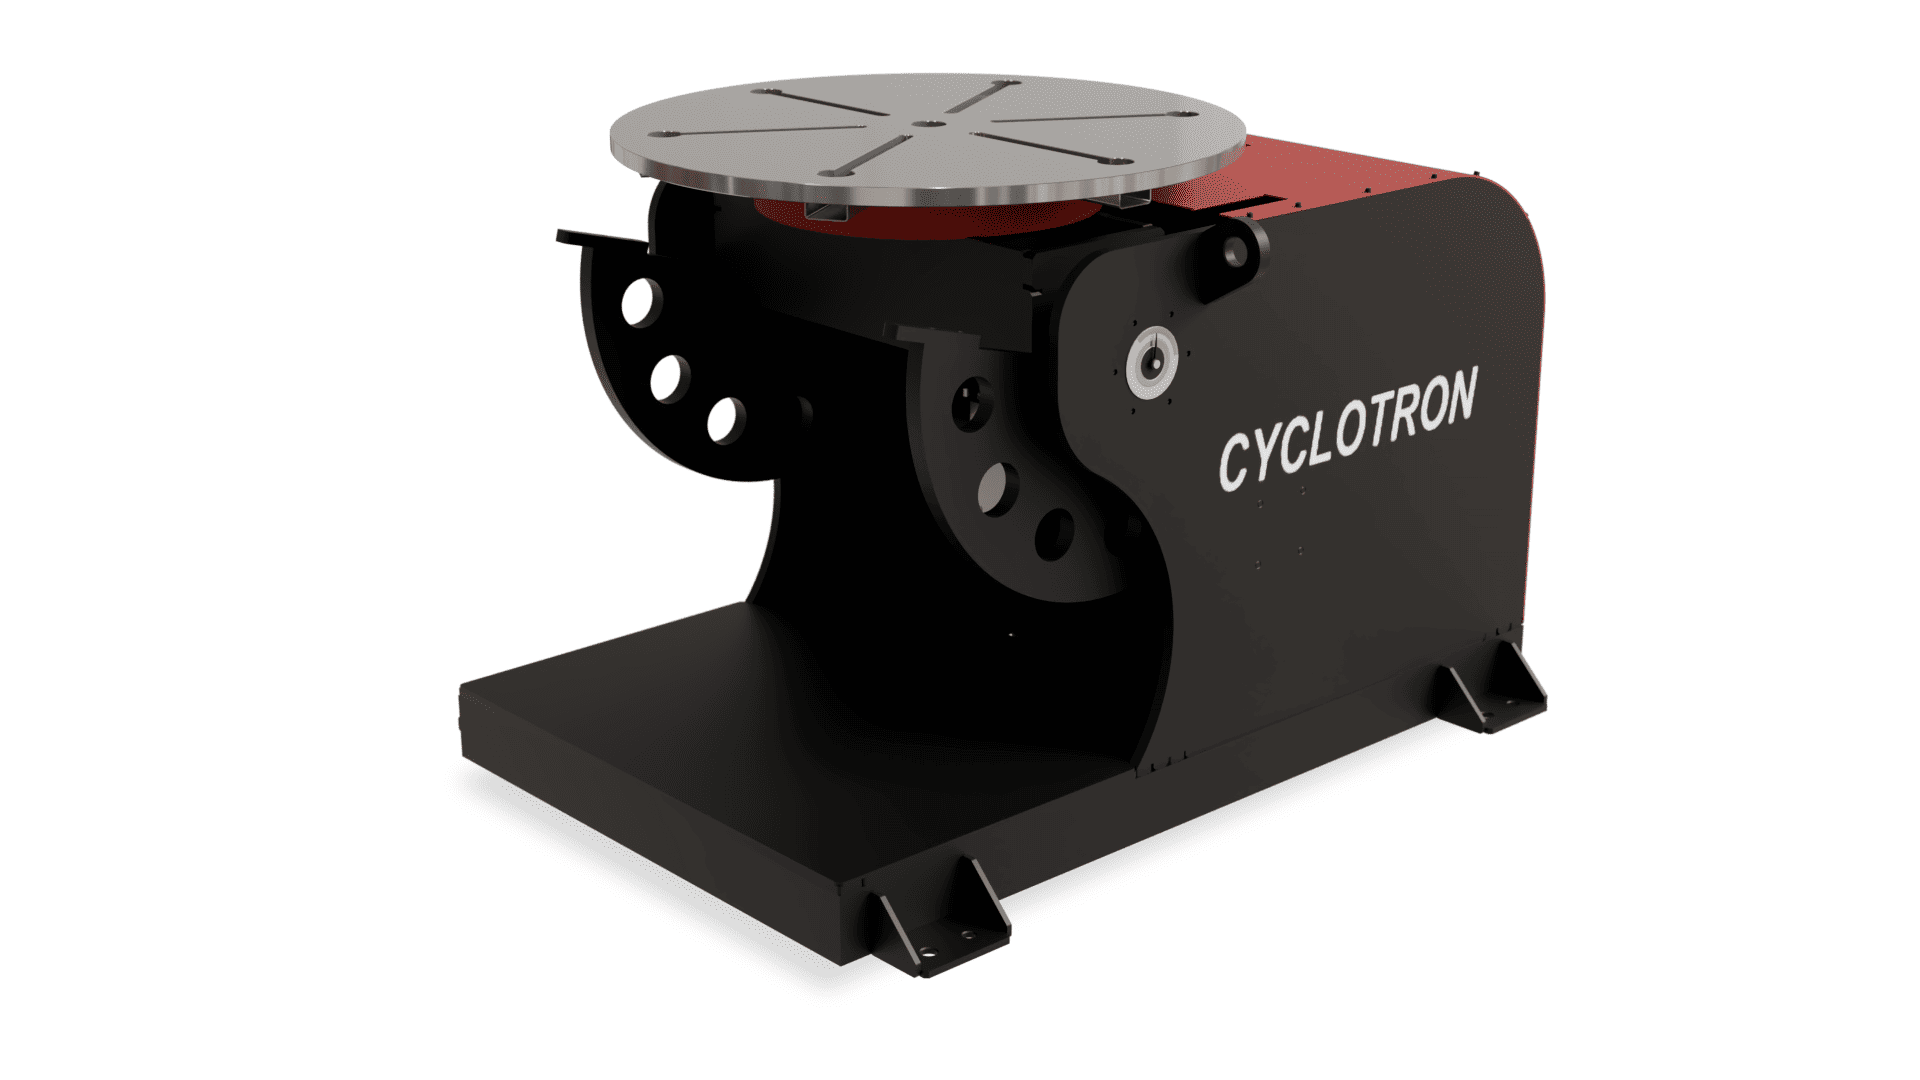
Universal welding positioner
SKU: CUP-2AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Tilting of face plate (0-135°)
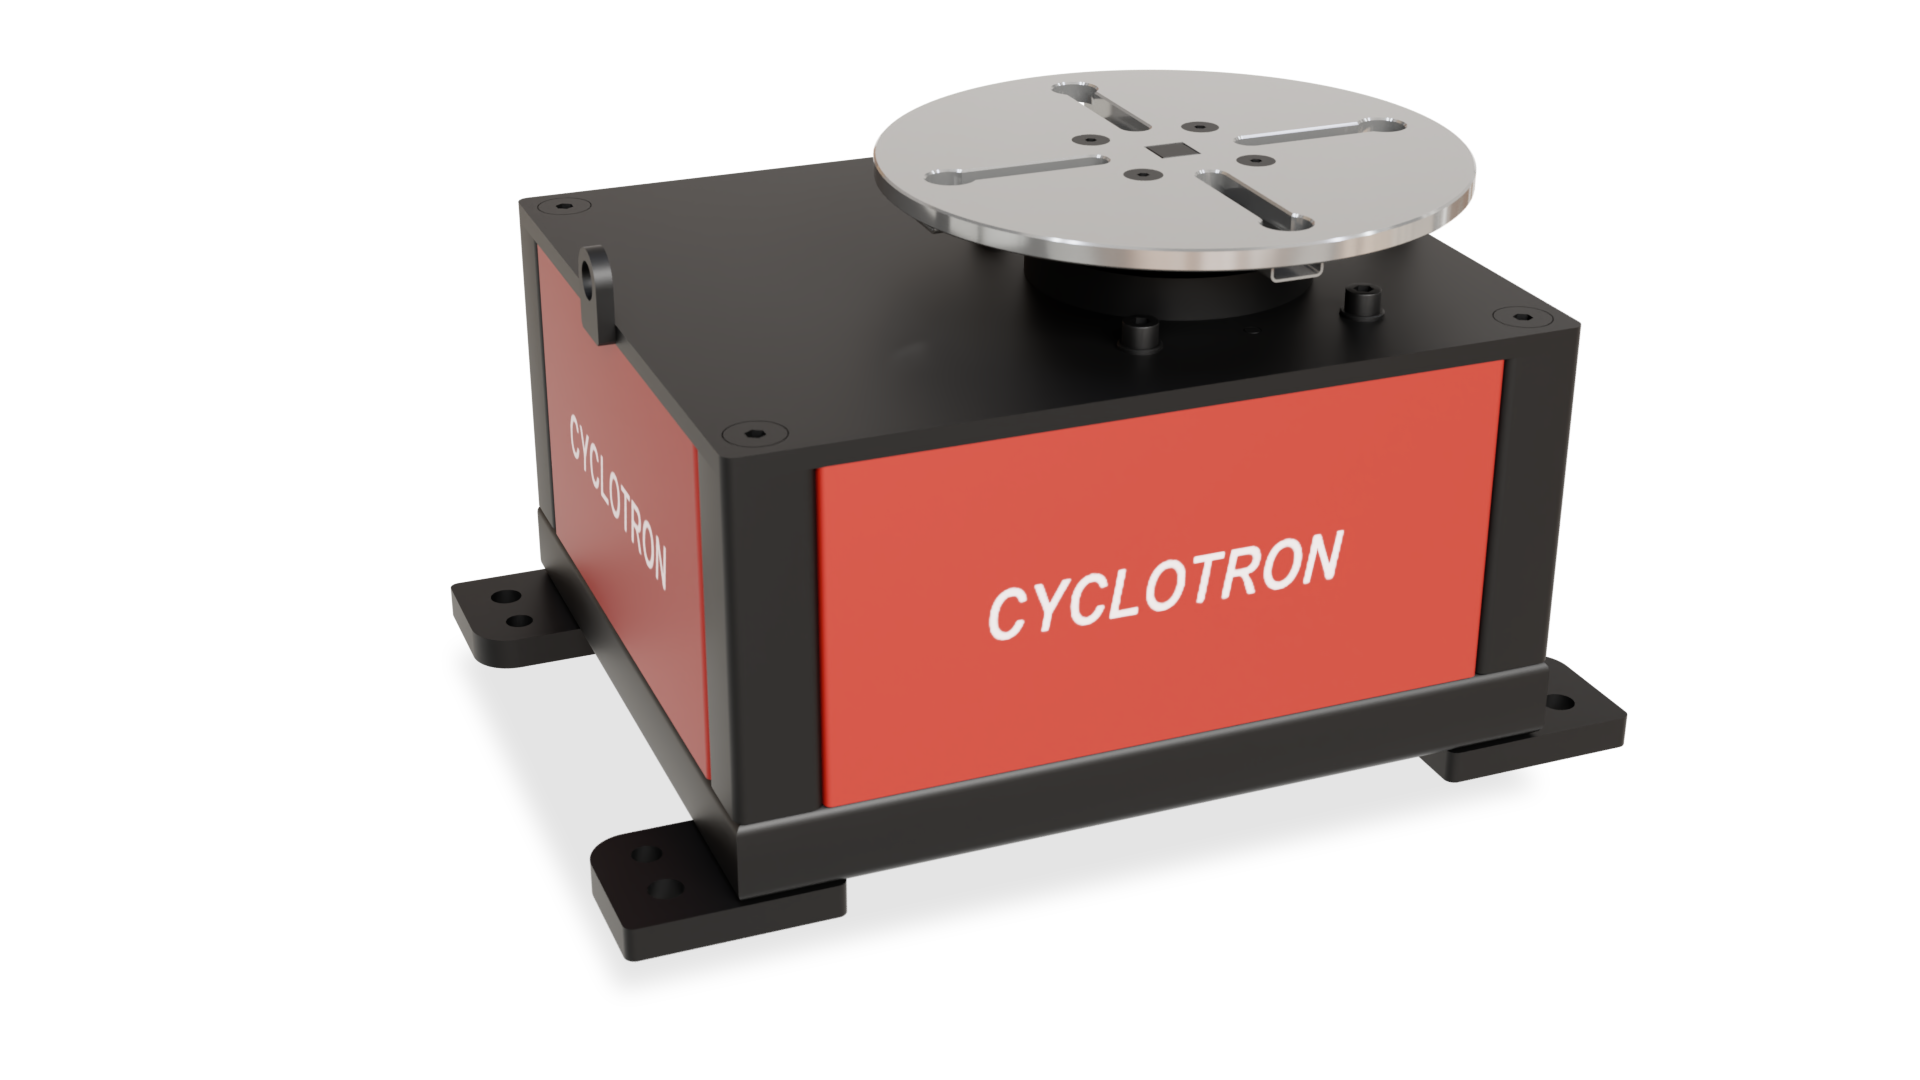
Mini Welding turntable
SKU: Mini-CTT-1AX
1st Axis: Face plate rotation (0-360°)
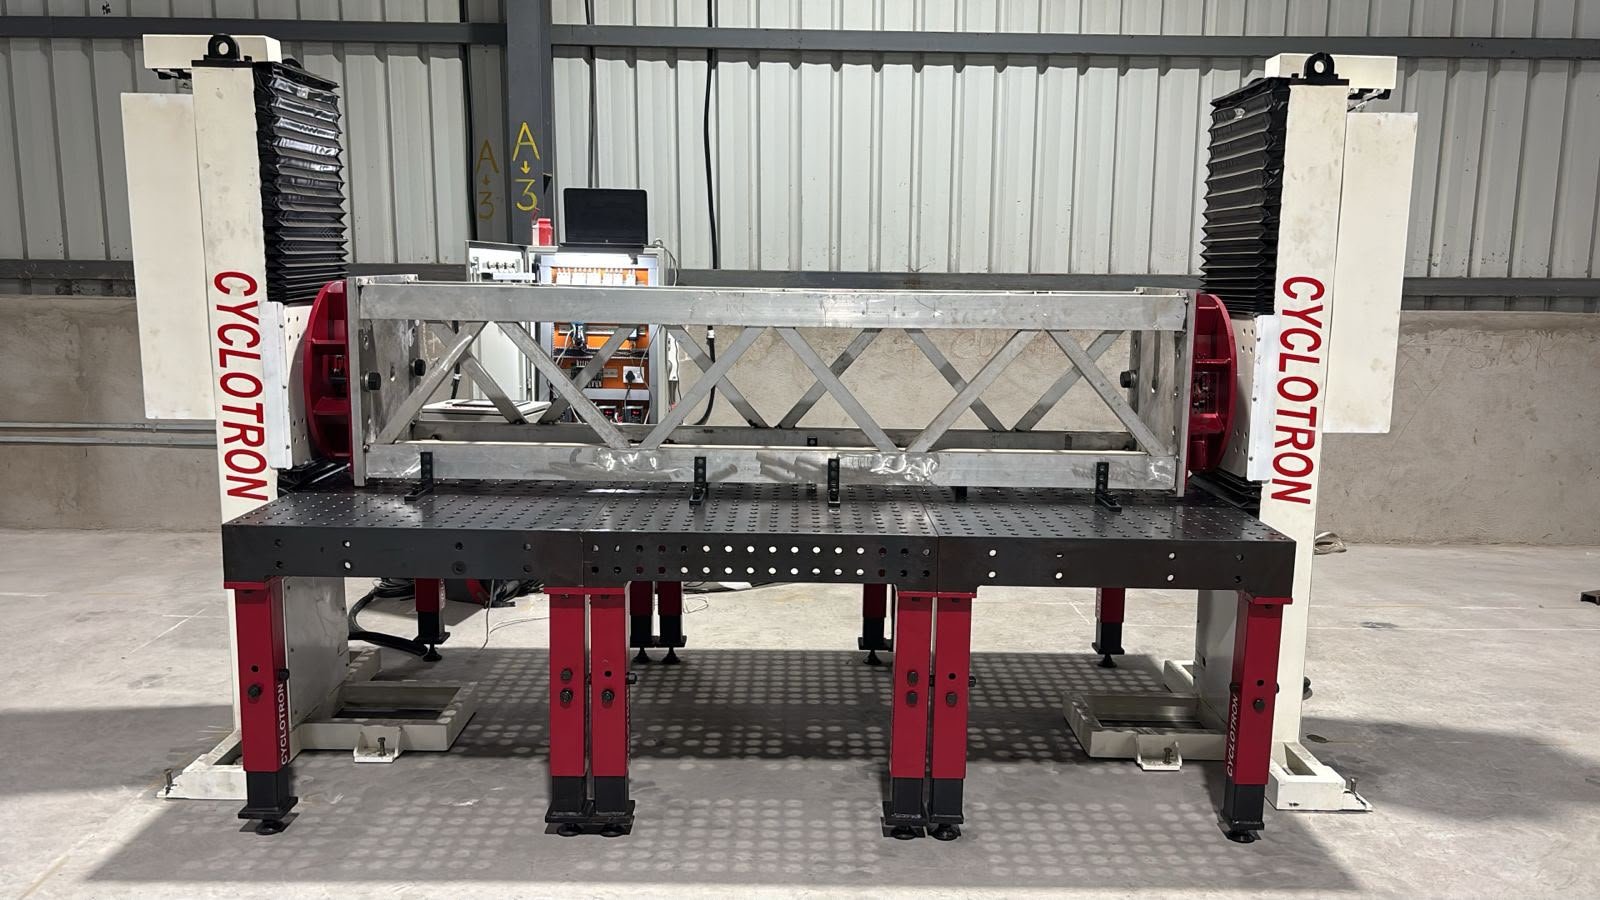
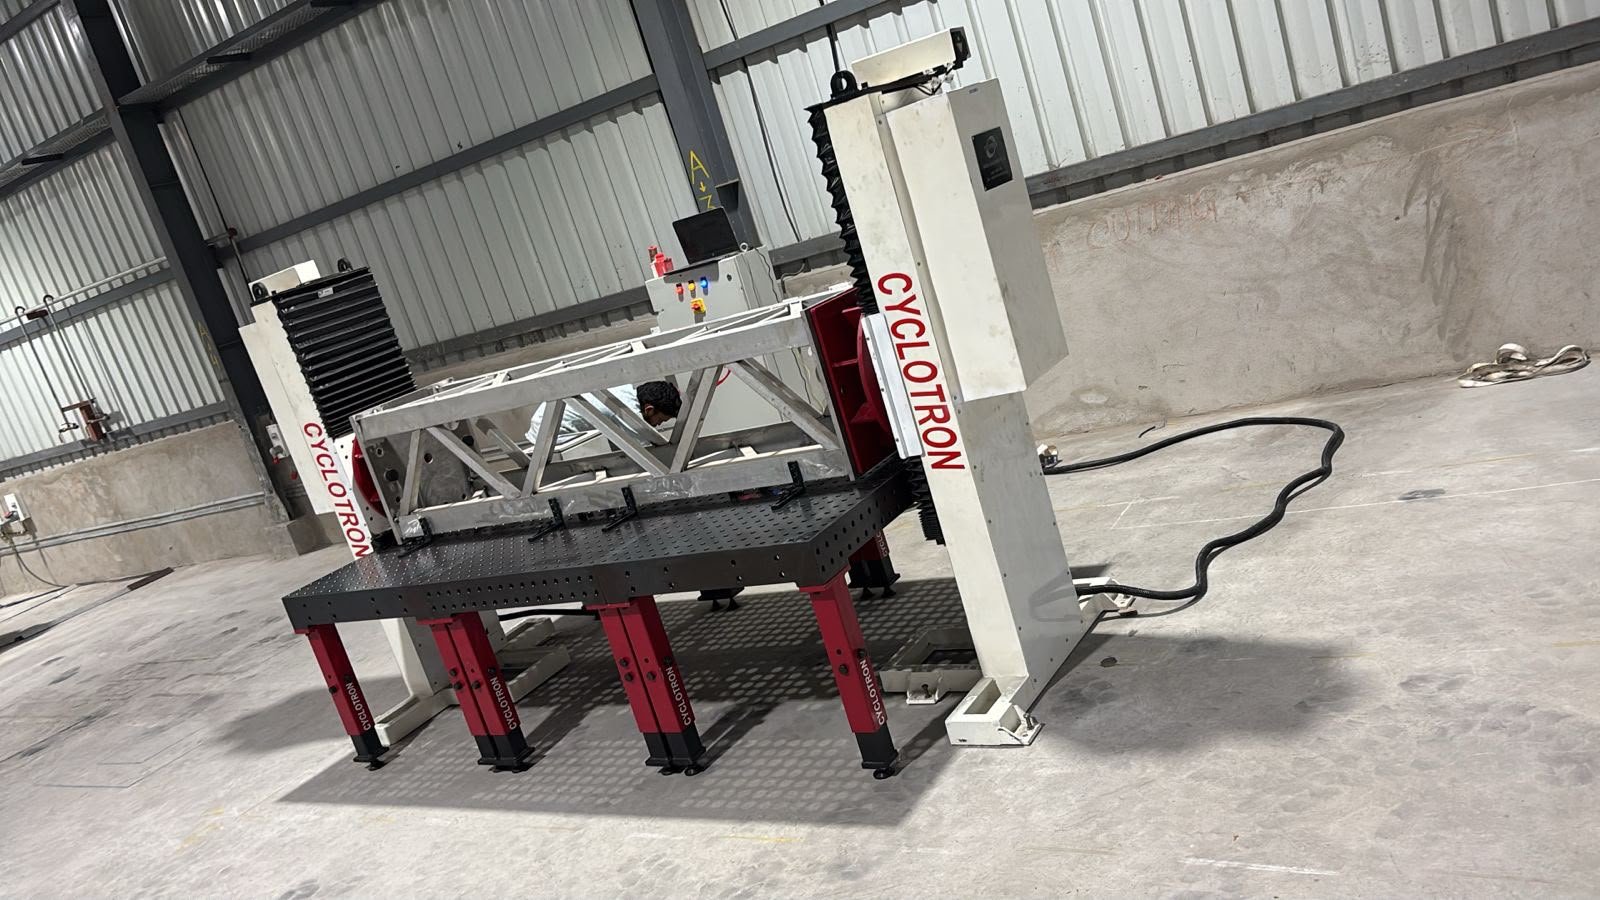
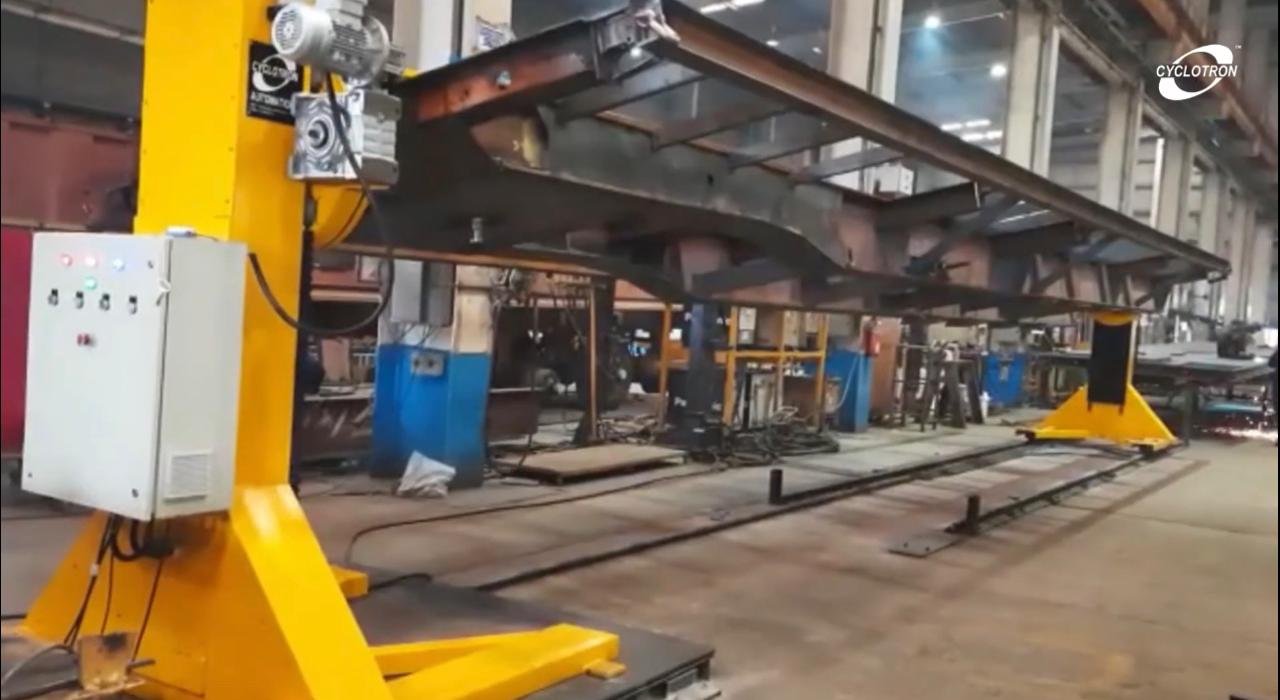
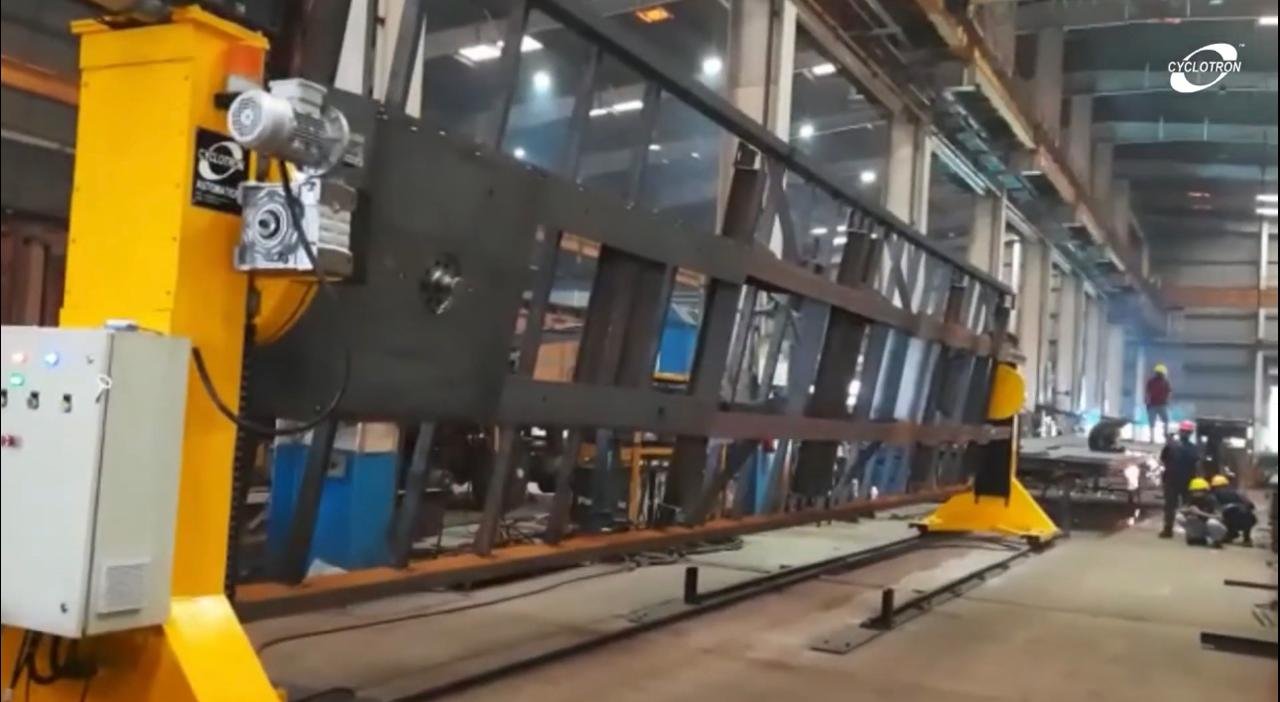
Headstock tailstock welding positioners in Hosur
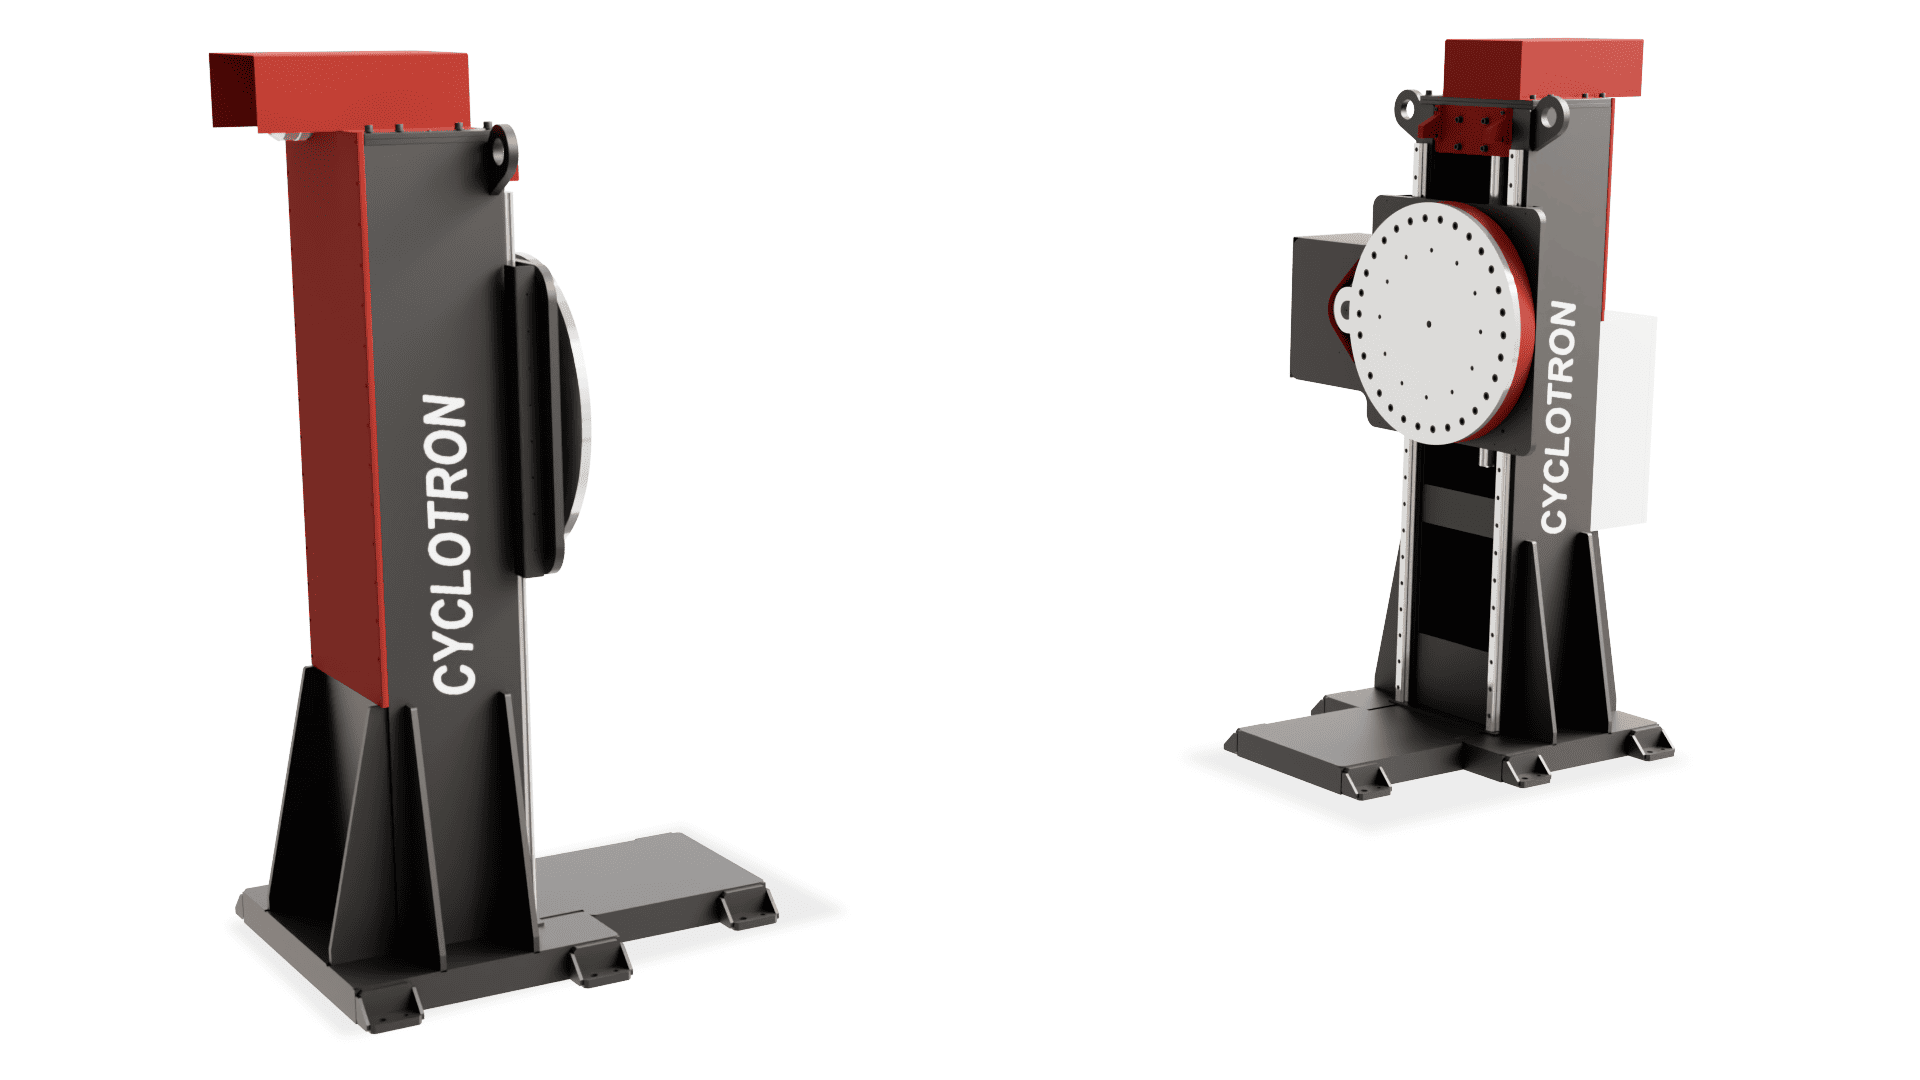
Headstock tailstock positioner-2 Axis
SKU: CY-HTP-2AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Height adjustment
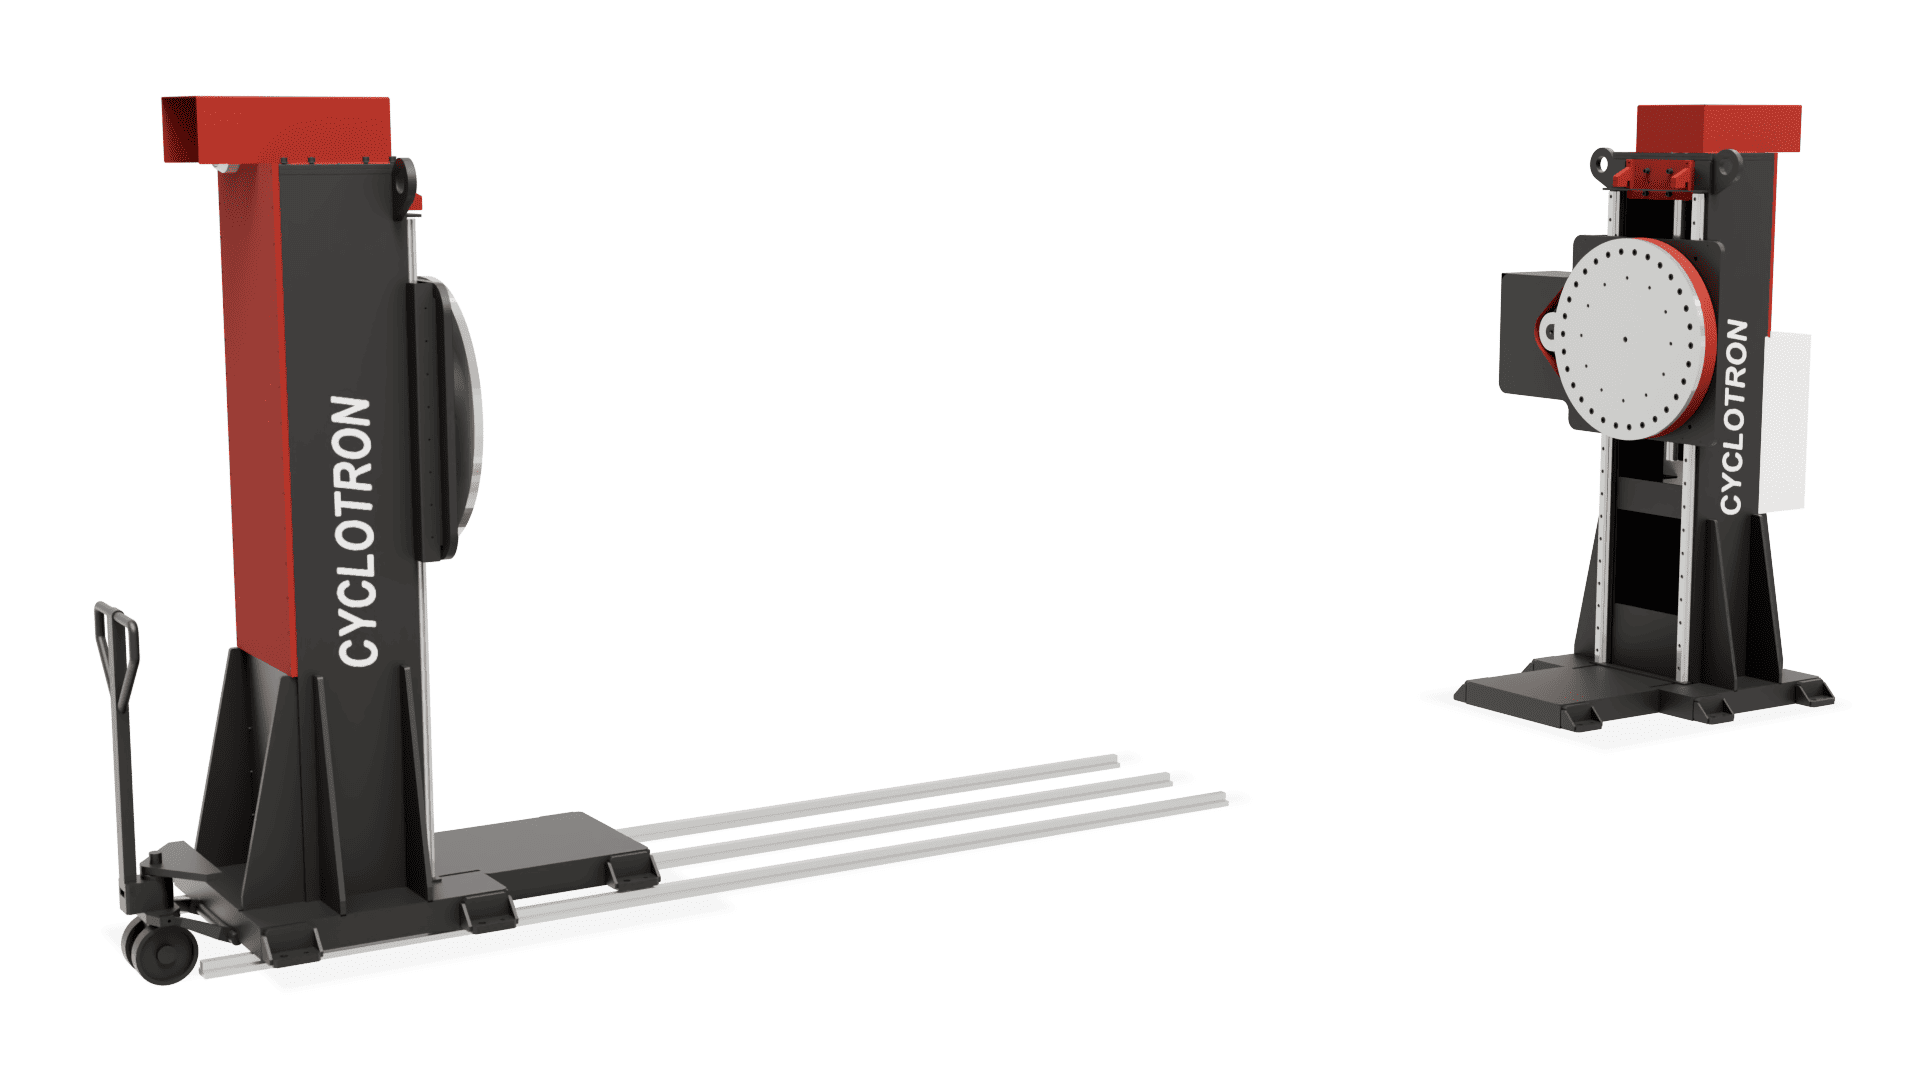
Headstock tailstock positioner-2 Axis with Rail
SKU: CY-HTP-2AX-R
1st Axis: Face plate rotation (0-360°)
2nd Axis: Height adjustment
Rail: Span between headstock and tailstock is adjustable
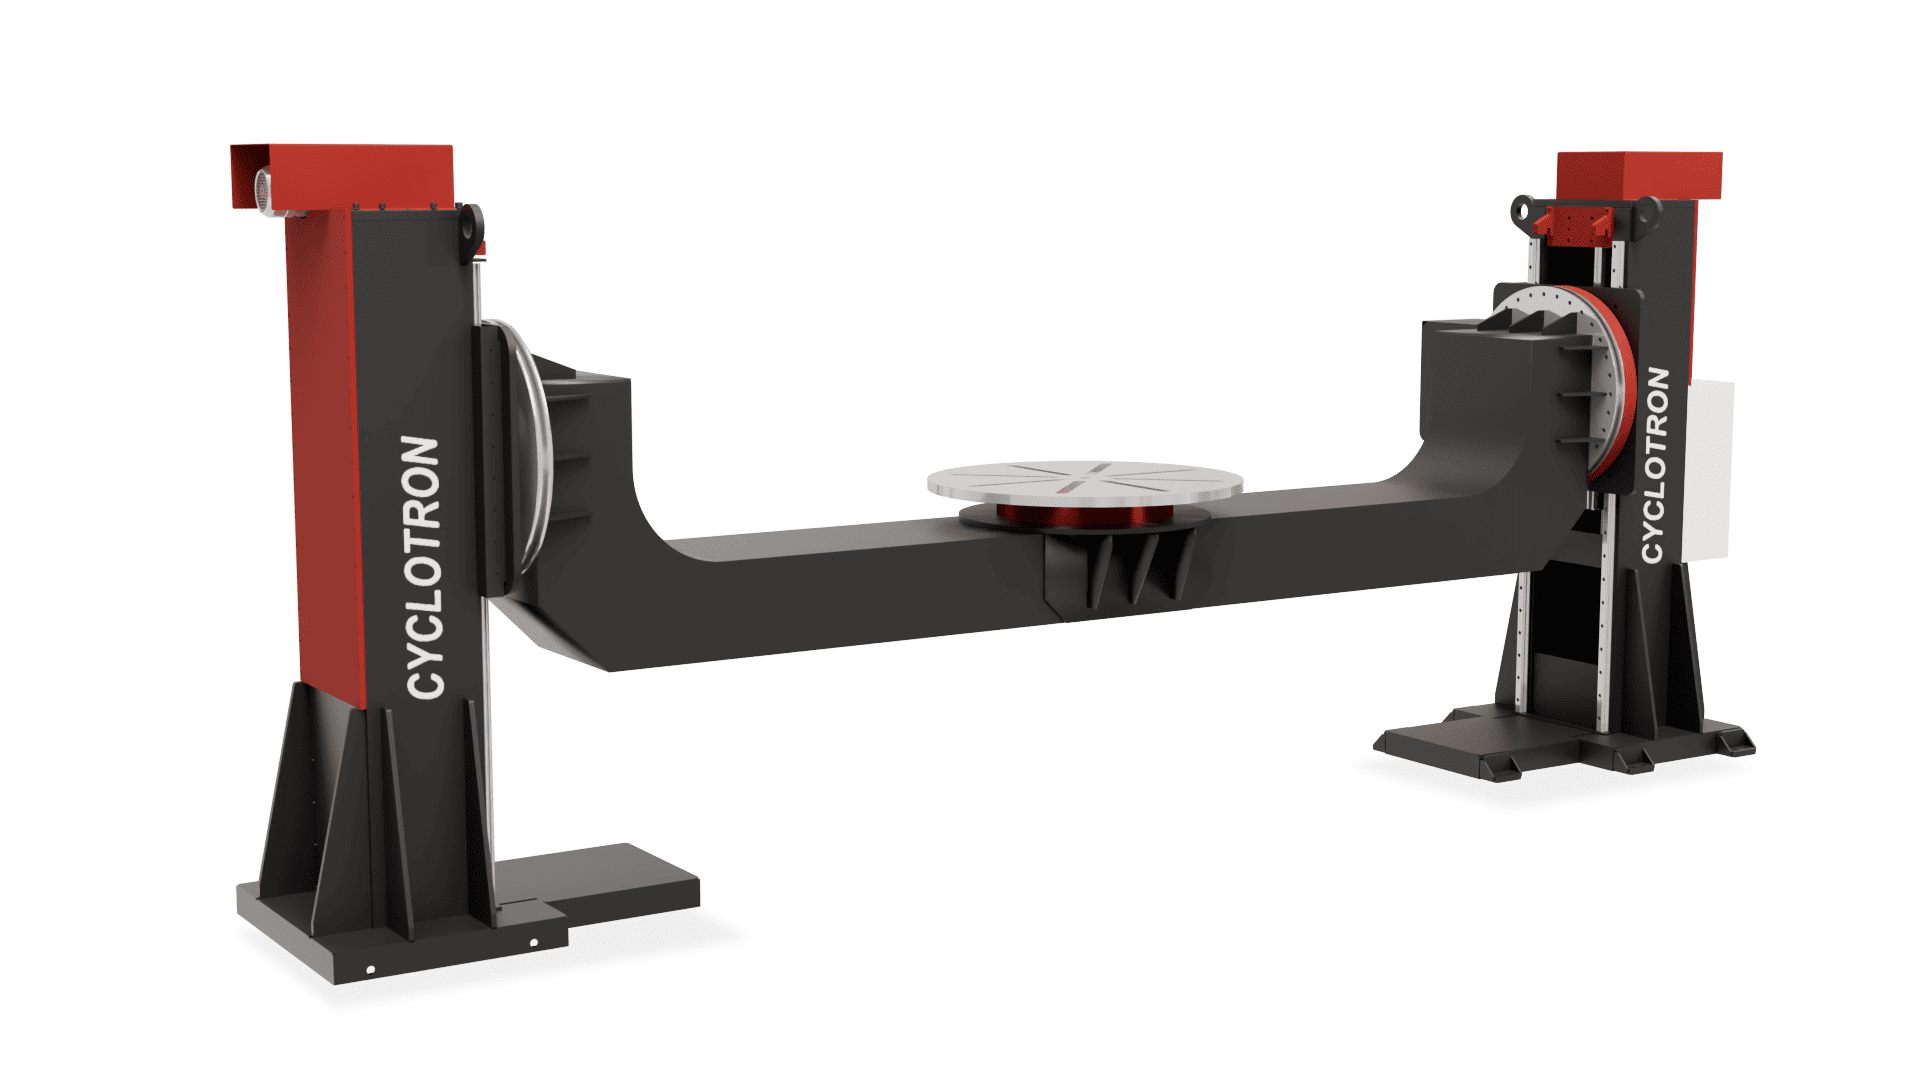
Headstock tailstock positioner-3 Axis
SKU: CY-HTP-3AX
1st Axis: Face plate rotation (0-360°)
2nd Axis: Tilting of the cradle (0-360°)
3rd Axis: Height adjustment
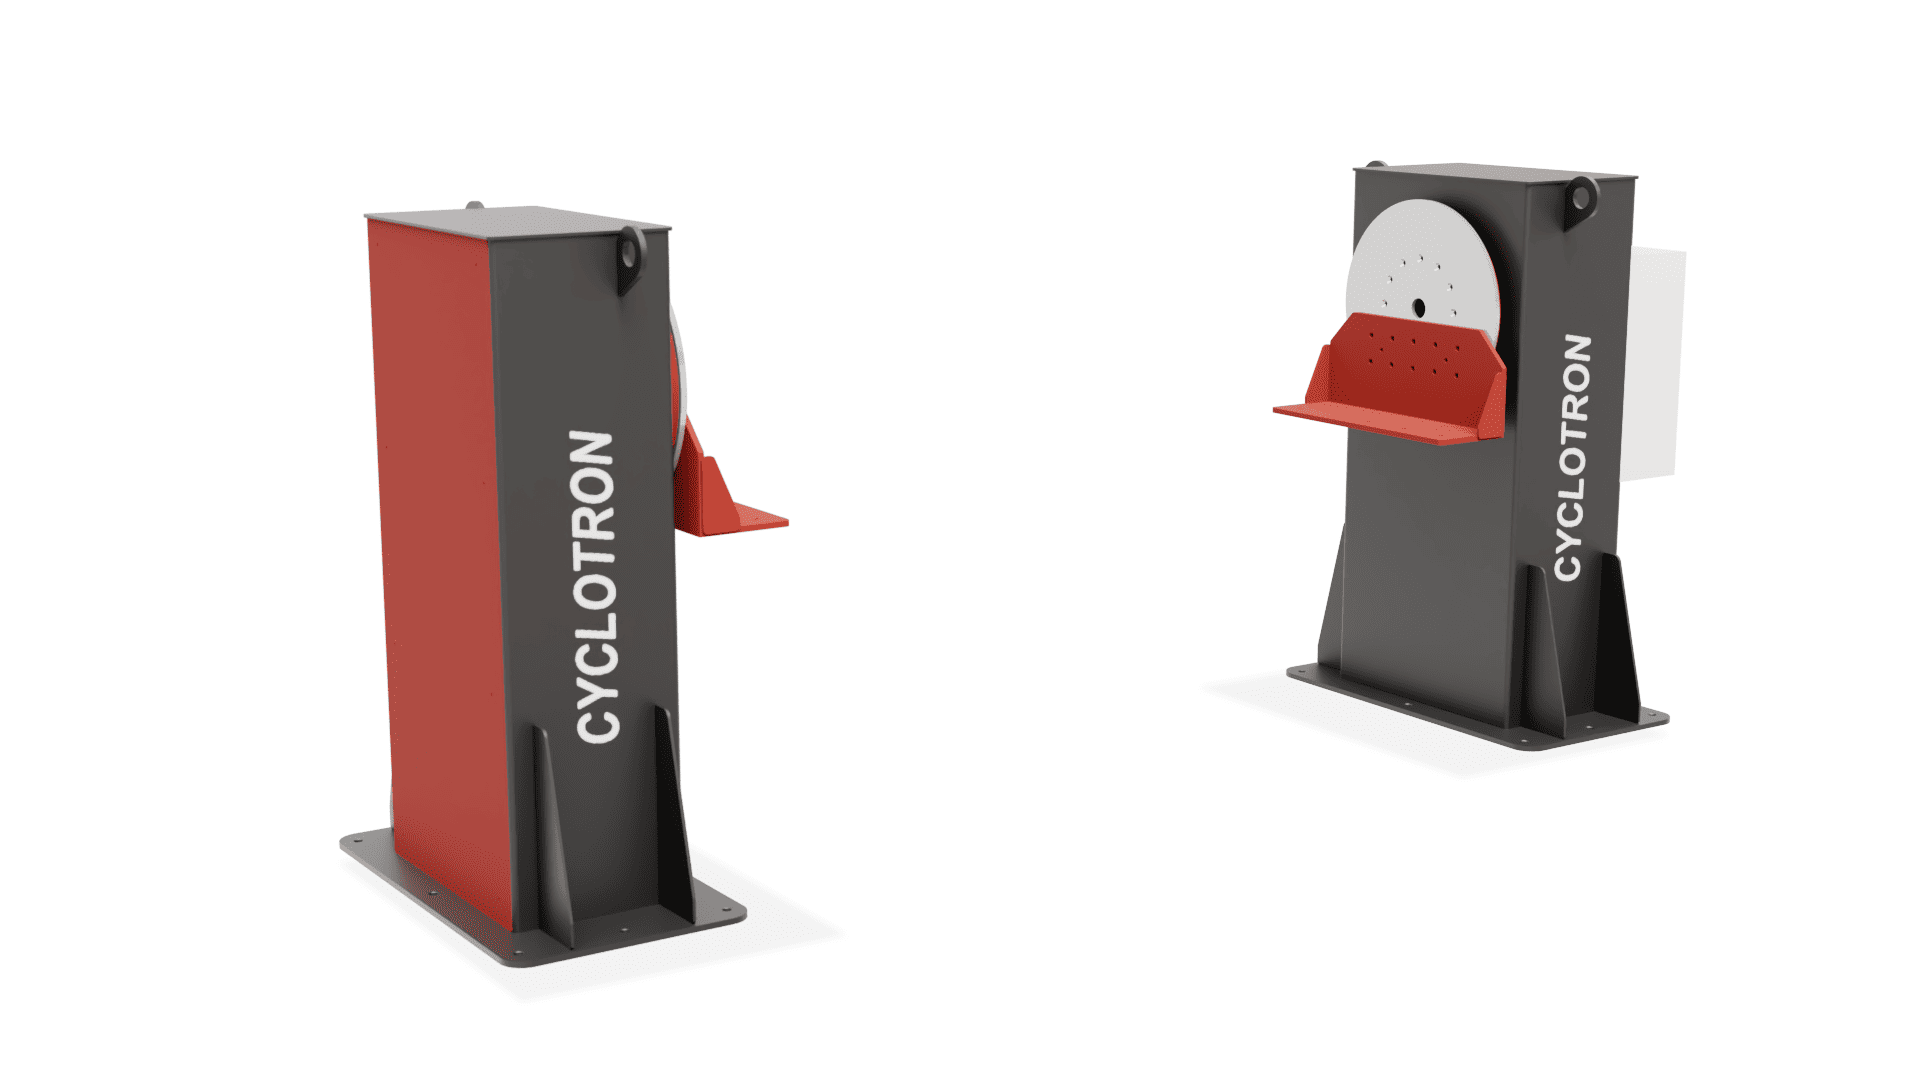
Headstock tailstock positioner-1 Axis
SKU: CY-HTP-1AX
1st Axis: Face plate rotation (0-360°)
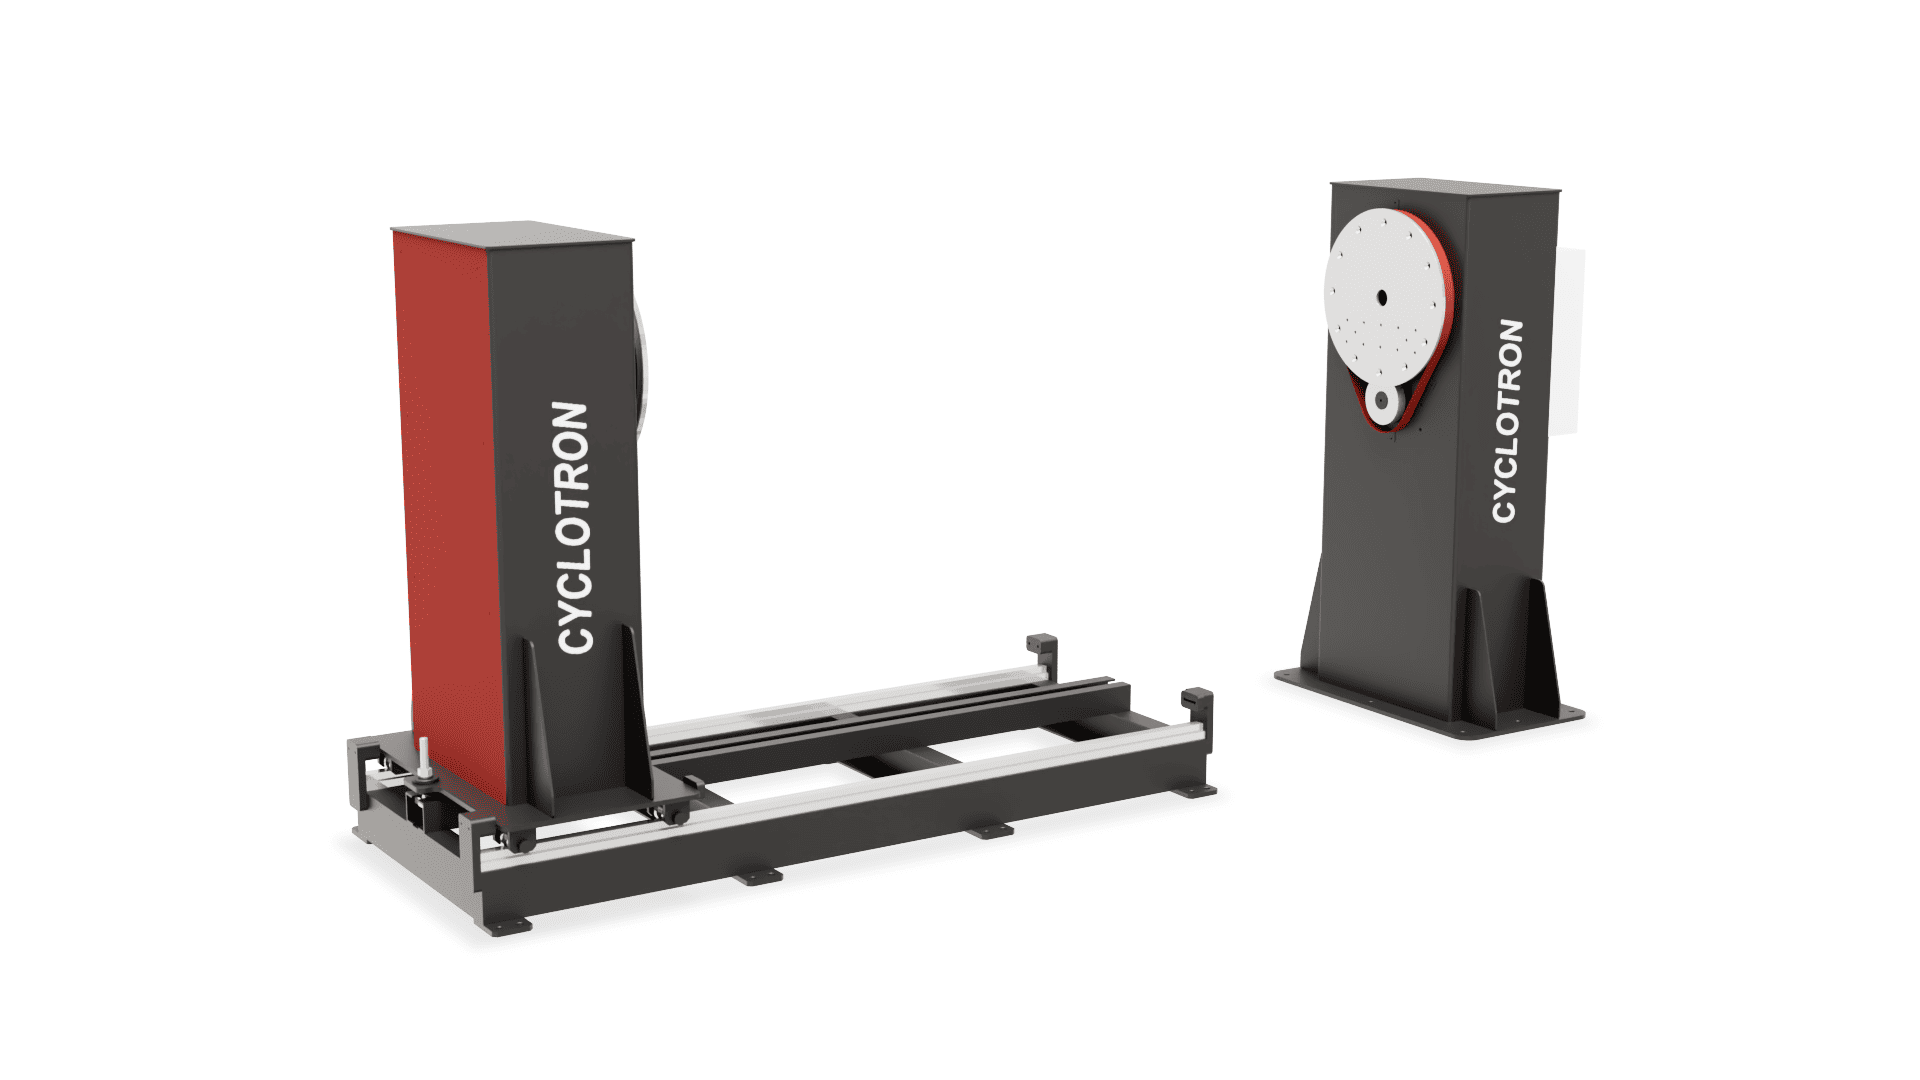
Headstock tailstock positioner-1 Axis with Rail
SKU: CY-HTP-1AX-R
1st Axis: Face plate rotation (0-360°)
Rail: Span between headstock and tailstock is adjustable
L type Welding Positioners in Hosur
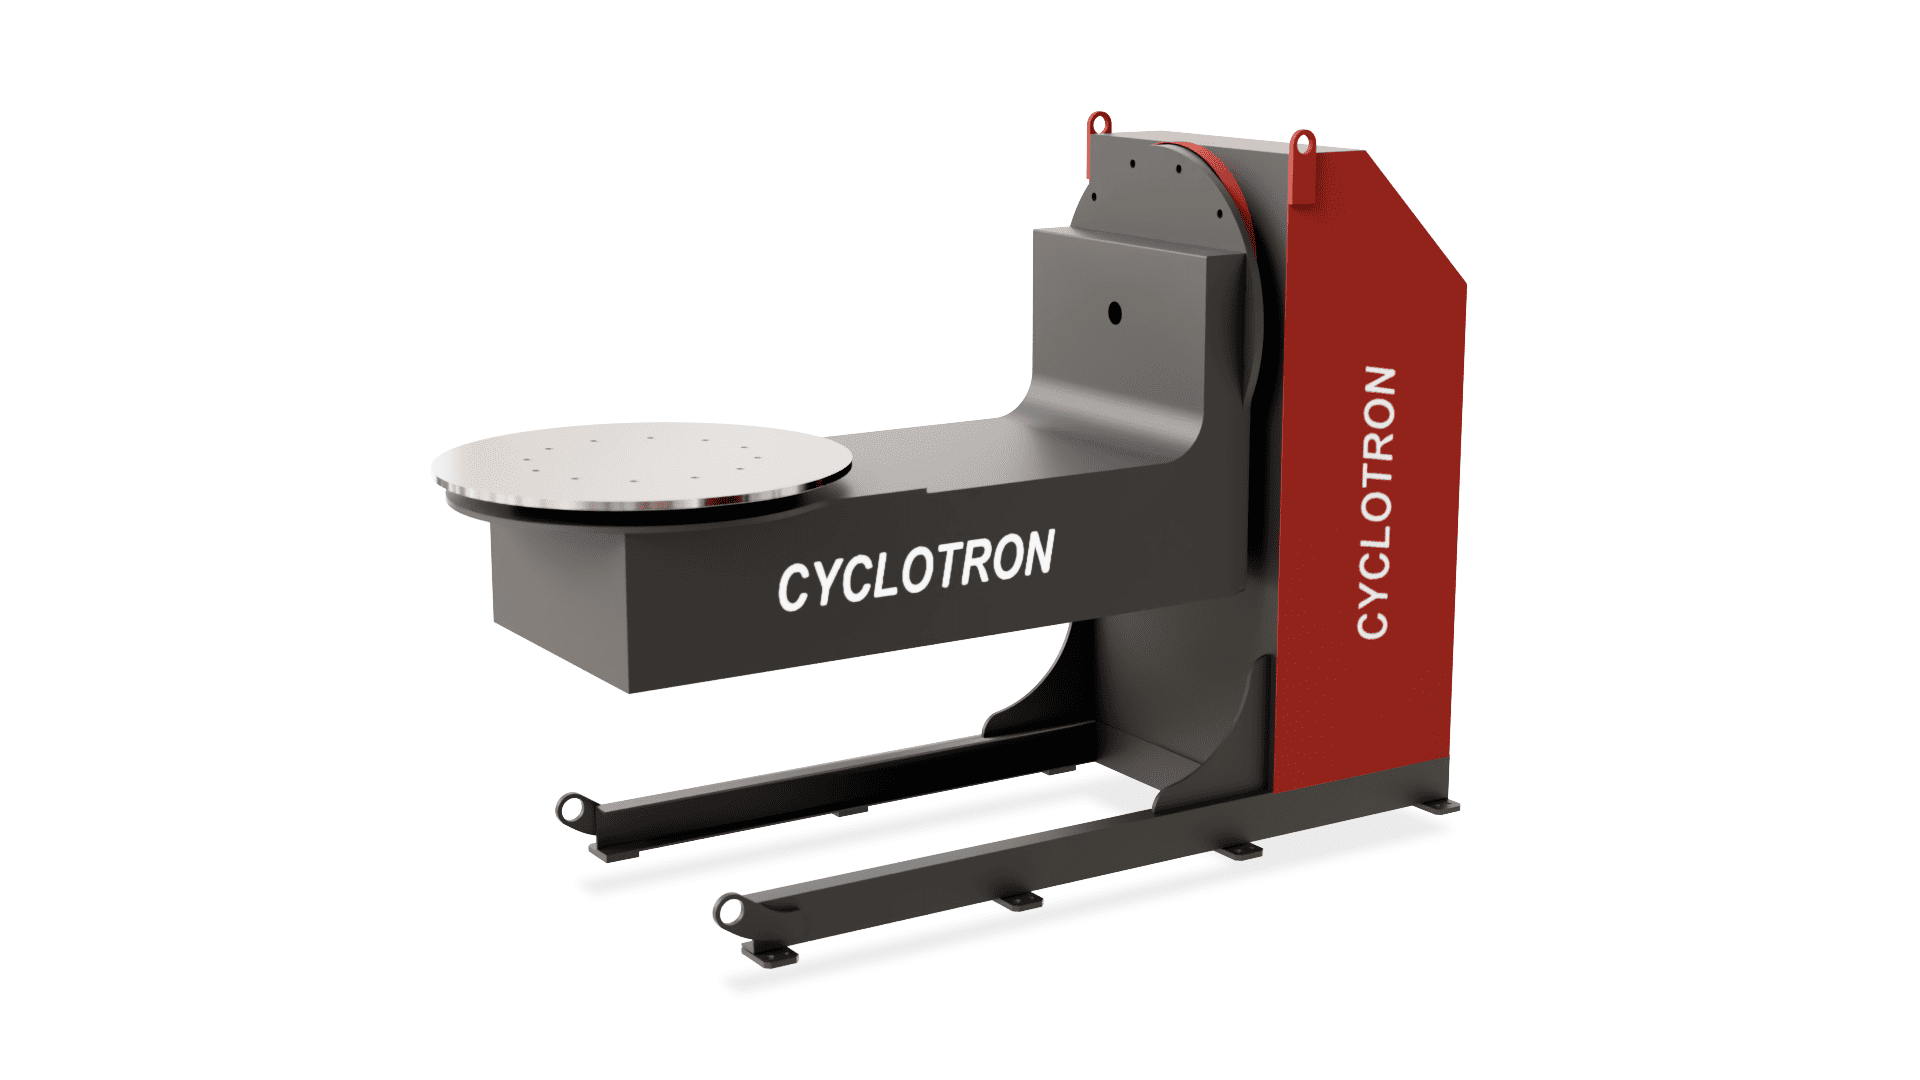
Cyclotron L Type Positioner 2AX
SKU: CLP-2AX
2 Axis (Rotation + Tilting)
Aluminium, Thin Gauge and Distortion Control using Positioners in Hosur
Aluminium and thin-section welding require careful control of heat input. Excessive or inconsistent heat can contribute to burn-through, distortion, and inconsistent penetration, particularly where the section is thin or the welding parameters are difficult to maintain.
Controlled rotation can help the welder maintain a more consistent travel speed and welding position around the component. A steady low-speed rotation is particularly relevant where the weld follows a circular or continuous path.
For EV battery enclosures, aluminium brackets and fabricated frames, the positioner’s ability to maintain controlled movement can therefore form part of the overall welding process.
The machine should be selected around the actual application, including:
- Material and section thickness
- Component weight and dimensions
- Required rotation speed
- Weld type and joint geometry
- Fixture arrangement
- Whether indexing or programmable positioning is required
A positioner does not eliminate distortion by itself. Welding parameters, joint design, fixturing and heat input still remain critical. The positioner’s role is to provide controlled and repeatable component movement as part of that process.
Two-Wheeler Ancillary and High-Volume Bracket Work
Hosur’s established two-wheeler ancillary sector creates another type of positioning requirement: small components produced repeatedly and often held in dedicated fixtures.
Brackets, frames, mounts and other fabricated components can be fixture-mounted on a turntable or positioner to maintain a consistent welding orientation from one part to the next.
For repetitive work, indexing can be useful where the component needs to stop at defined positions for successive welds. A suitable fixture combined with repeatable positioning can reduce manual repositioning between operations.
For applications requiring simple continuous rotation, a [Welding Turntable] may be sufficient. Wherever the application requires defined positions or additional axis movement, a more advanced positioner can be considered
Why Hosur Shops Specify Servo Over VFD
Servo and VFD systems solve different problems, so servo is not automatically the better choice.
A VFD (Variable Frequency Drive) controls motor speed by varying the frequency supplied to the motor. It can be a practical solution where the requirement is straightforward variable-speed rotation and precise axis positioning is not required.
A servo system adds feedback, allowing the control system to monitor and control the motor’s position. This makes servo more relevant where the application requires repeatable indexing, defined positioning or integration with an automated welding system.
The additional cost of servo is therefore easier to justify when positioning accuracy and automation are important.
For simple manual welding where the operator only needs smooth variable-speed rotation, VFD control may be sufficient.
Cyclotron’s Service Coverage: Hosur and Bangalore
Hosur and Bangalore can be covered through the same engineering service network.
Service response time: 24-72 hours
Our service support includes installation assistance, troubleshooting and spare-parts support, based on the agreed scope and machine configuration.
Spares availability: within 24-72 hours
For customers operating across the Hosur-Bangalore manufacturing corridor, having a defined service arrangement before purchase can be as important as the machine specification itself.
FAQs
Are Cyclotron positioners suitable for aluminium welding?
Yes, provided the selected positioner meets the application’s requirements. Controlled low-speed rotation can support consistent component movement during aluminium welding. However, the positioner alone does not prevent distortion or guarantee weld quality. Results still depend on heat input, joint design, welding parameters and fixturing.
What is the difference between VFD and servo rotation control?
A VFD primarily provides variable motor speed. A servo system uses feedback to control motor position as well as movement. VFD can be sufficient for straightforward variable-speed rotation, while servo is more appropriate when repeatable indexing, defined positioning or robotic integration is required.
Do you cover Hosur from Bangalore or from Pune?
Hosur is approximately 40 km from Bangalore, and both locations can be covered through our same engineering network.